I will verify Y axis when I get home but it looks like according to the info that was out there, I will get into config.yaml and adjust from 40 to 39.65 (was originally at 50 and I had wrong pulleys ) and should be close to home. Looked overwhelming at first but makes more sense now.
Yeah, it is not that bad, worst case is you go the wrong direction and just save and boot with new numbers. After you do the first one, it is no big deal. If you get stuck, we got you!!
Worked like a charm… seemed to be right on track using my cheap digital calipers.
A bit more foam work before I get brave enough to run my part. If I destroy it, should be easy enough to make a new one.
Test cuts are awesome, when you feel ready make the change to the bit breaker material. 
Was able to make the cut successfully! had one slight unexpected boo-boo but a little bit of putty should hide my error… I did not see a tab here to add a pic.
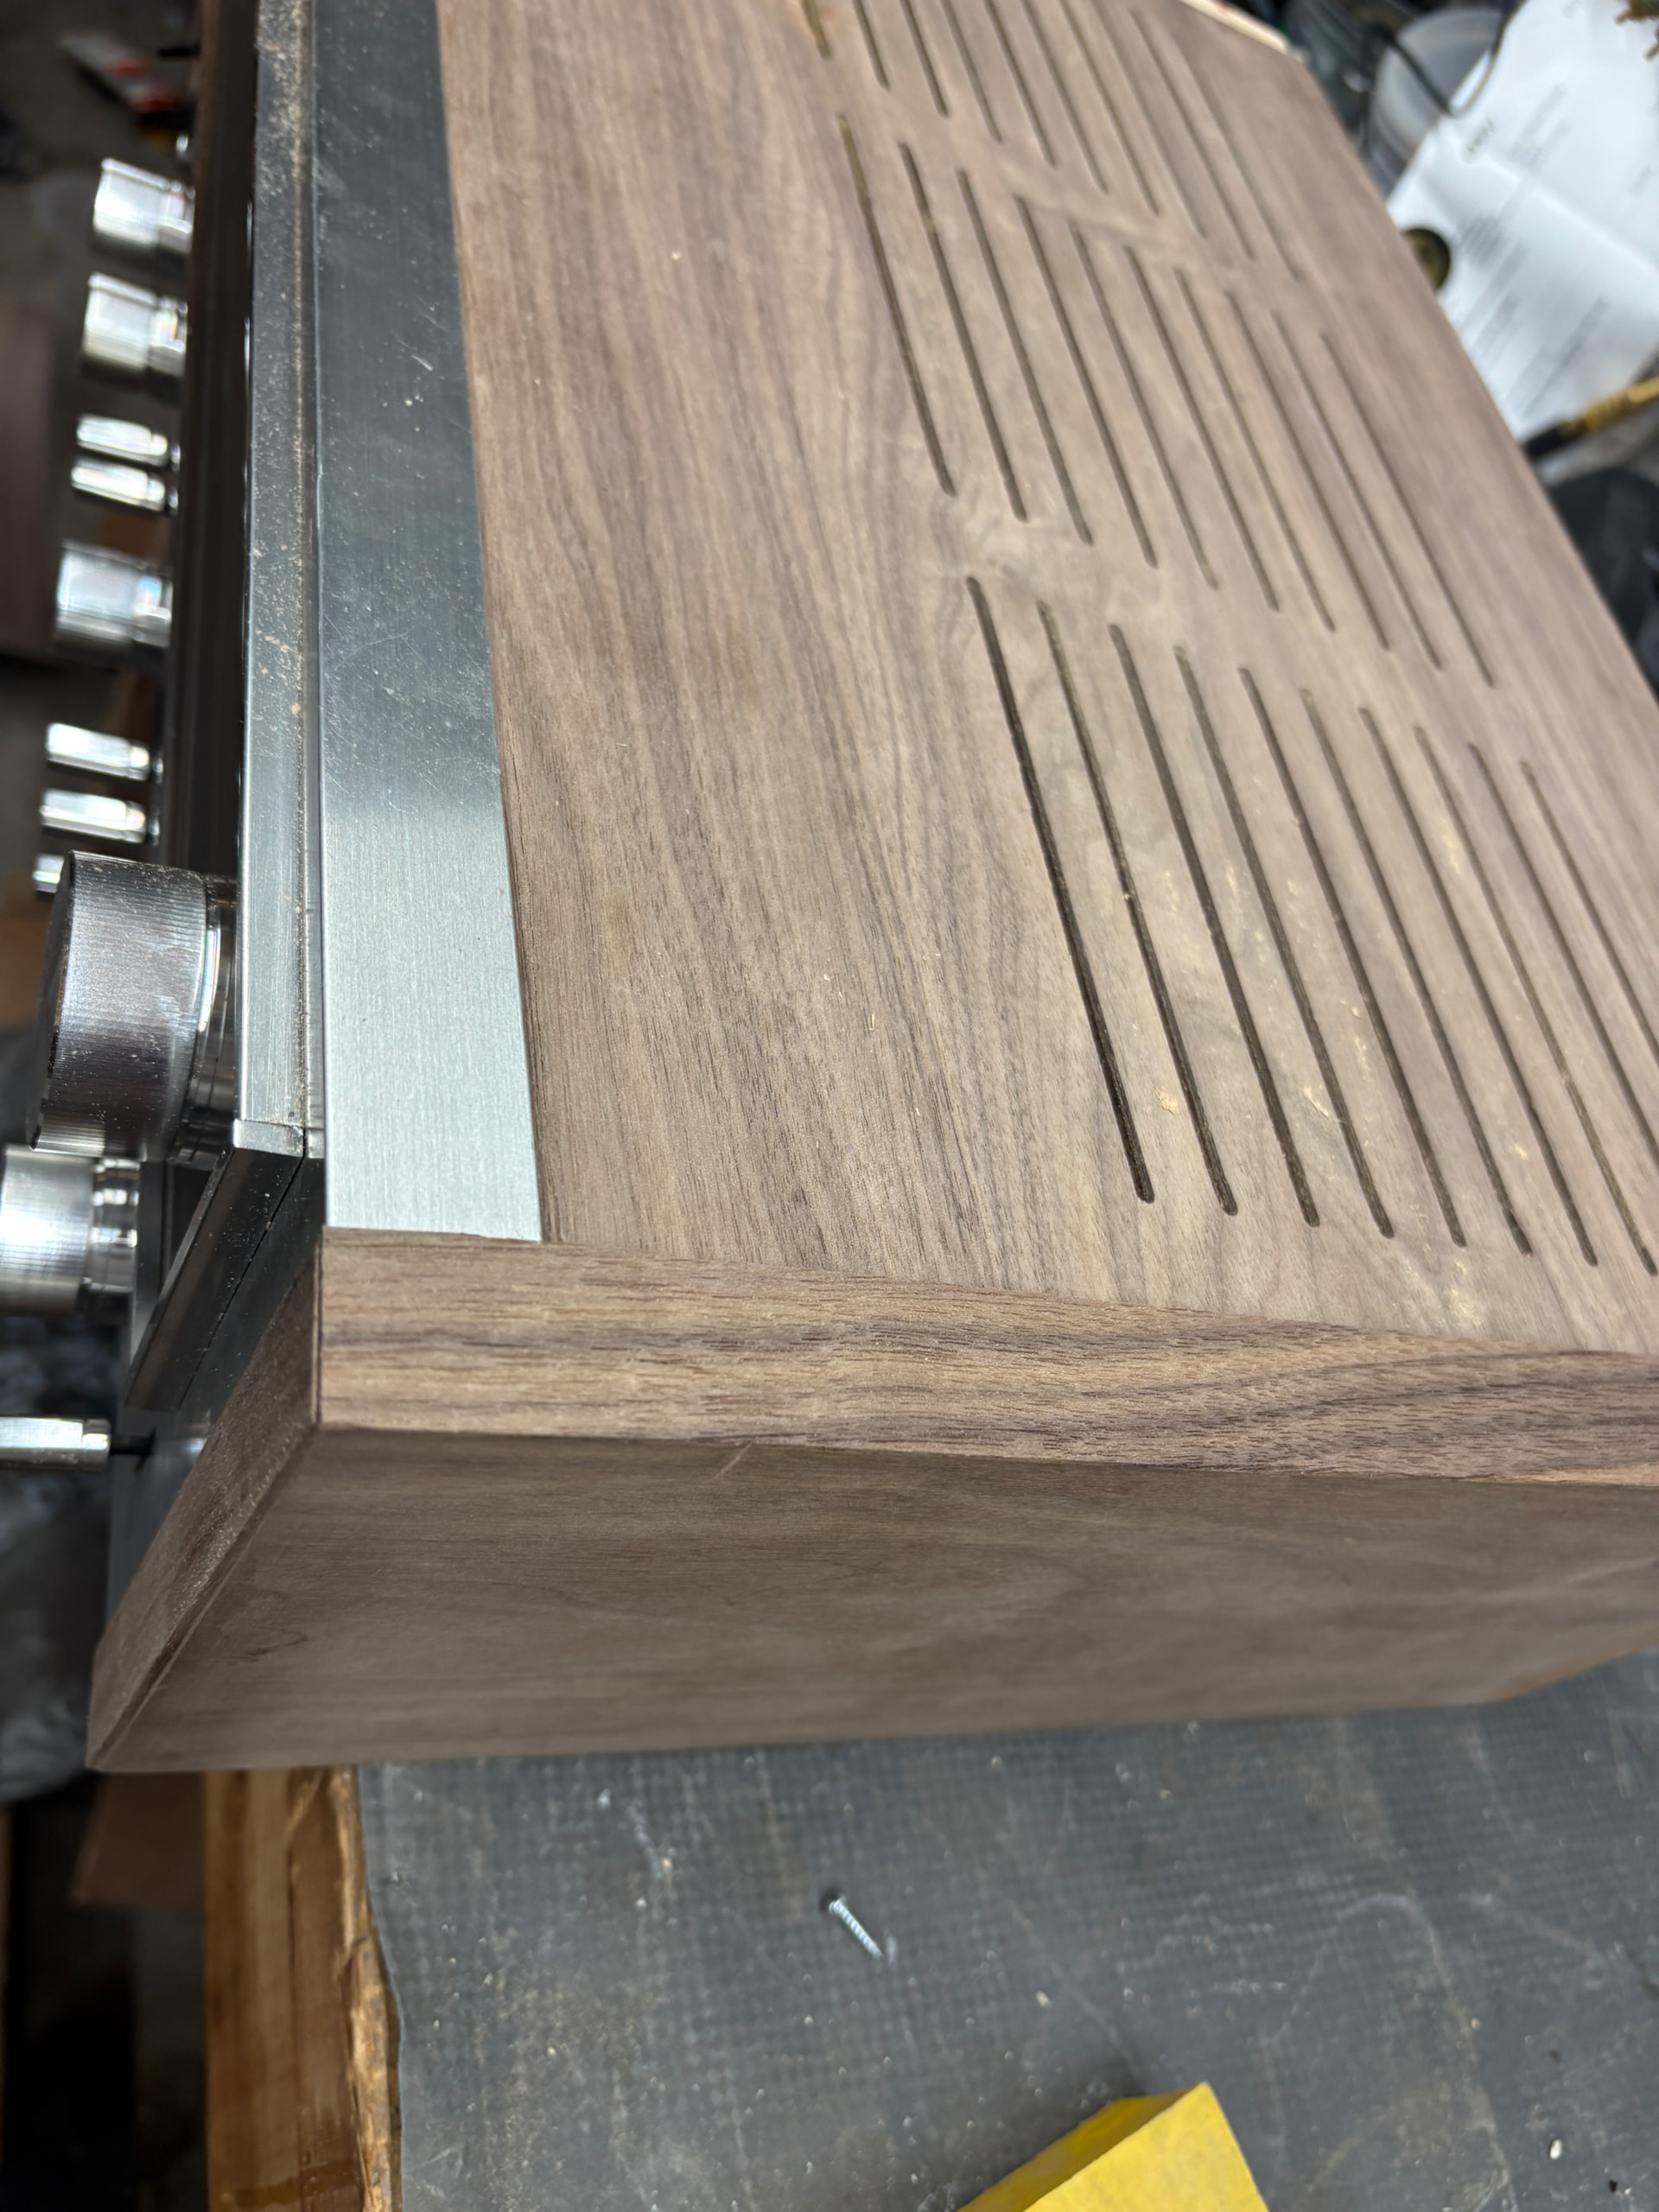
That looks really nice.
Taking a closer look… although delighted that it worked at all I can see some obvious drifting… and pretty sure it comes down to my Y axis right side belt being a bit looser than the others. Not sure how well this will show in the pic but several slots go a bit wonky at the ends. Might even tighten it up, and run it again with with a larger bit.
Noticed something strange. Every other row is a bit wonky, does not seem random. How could that be?
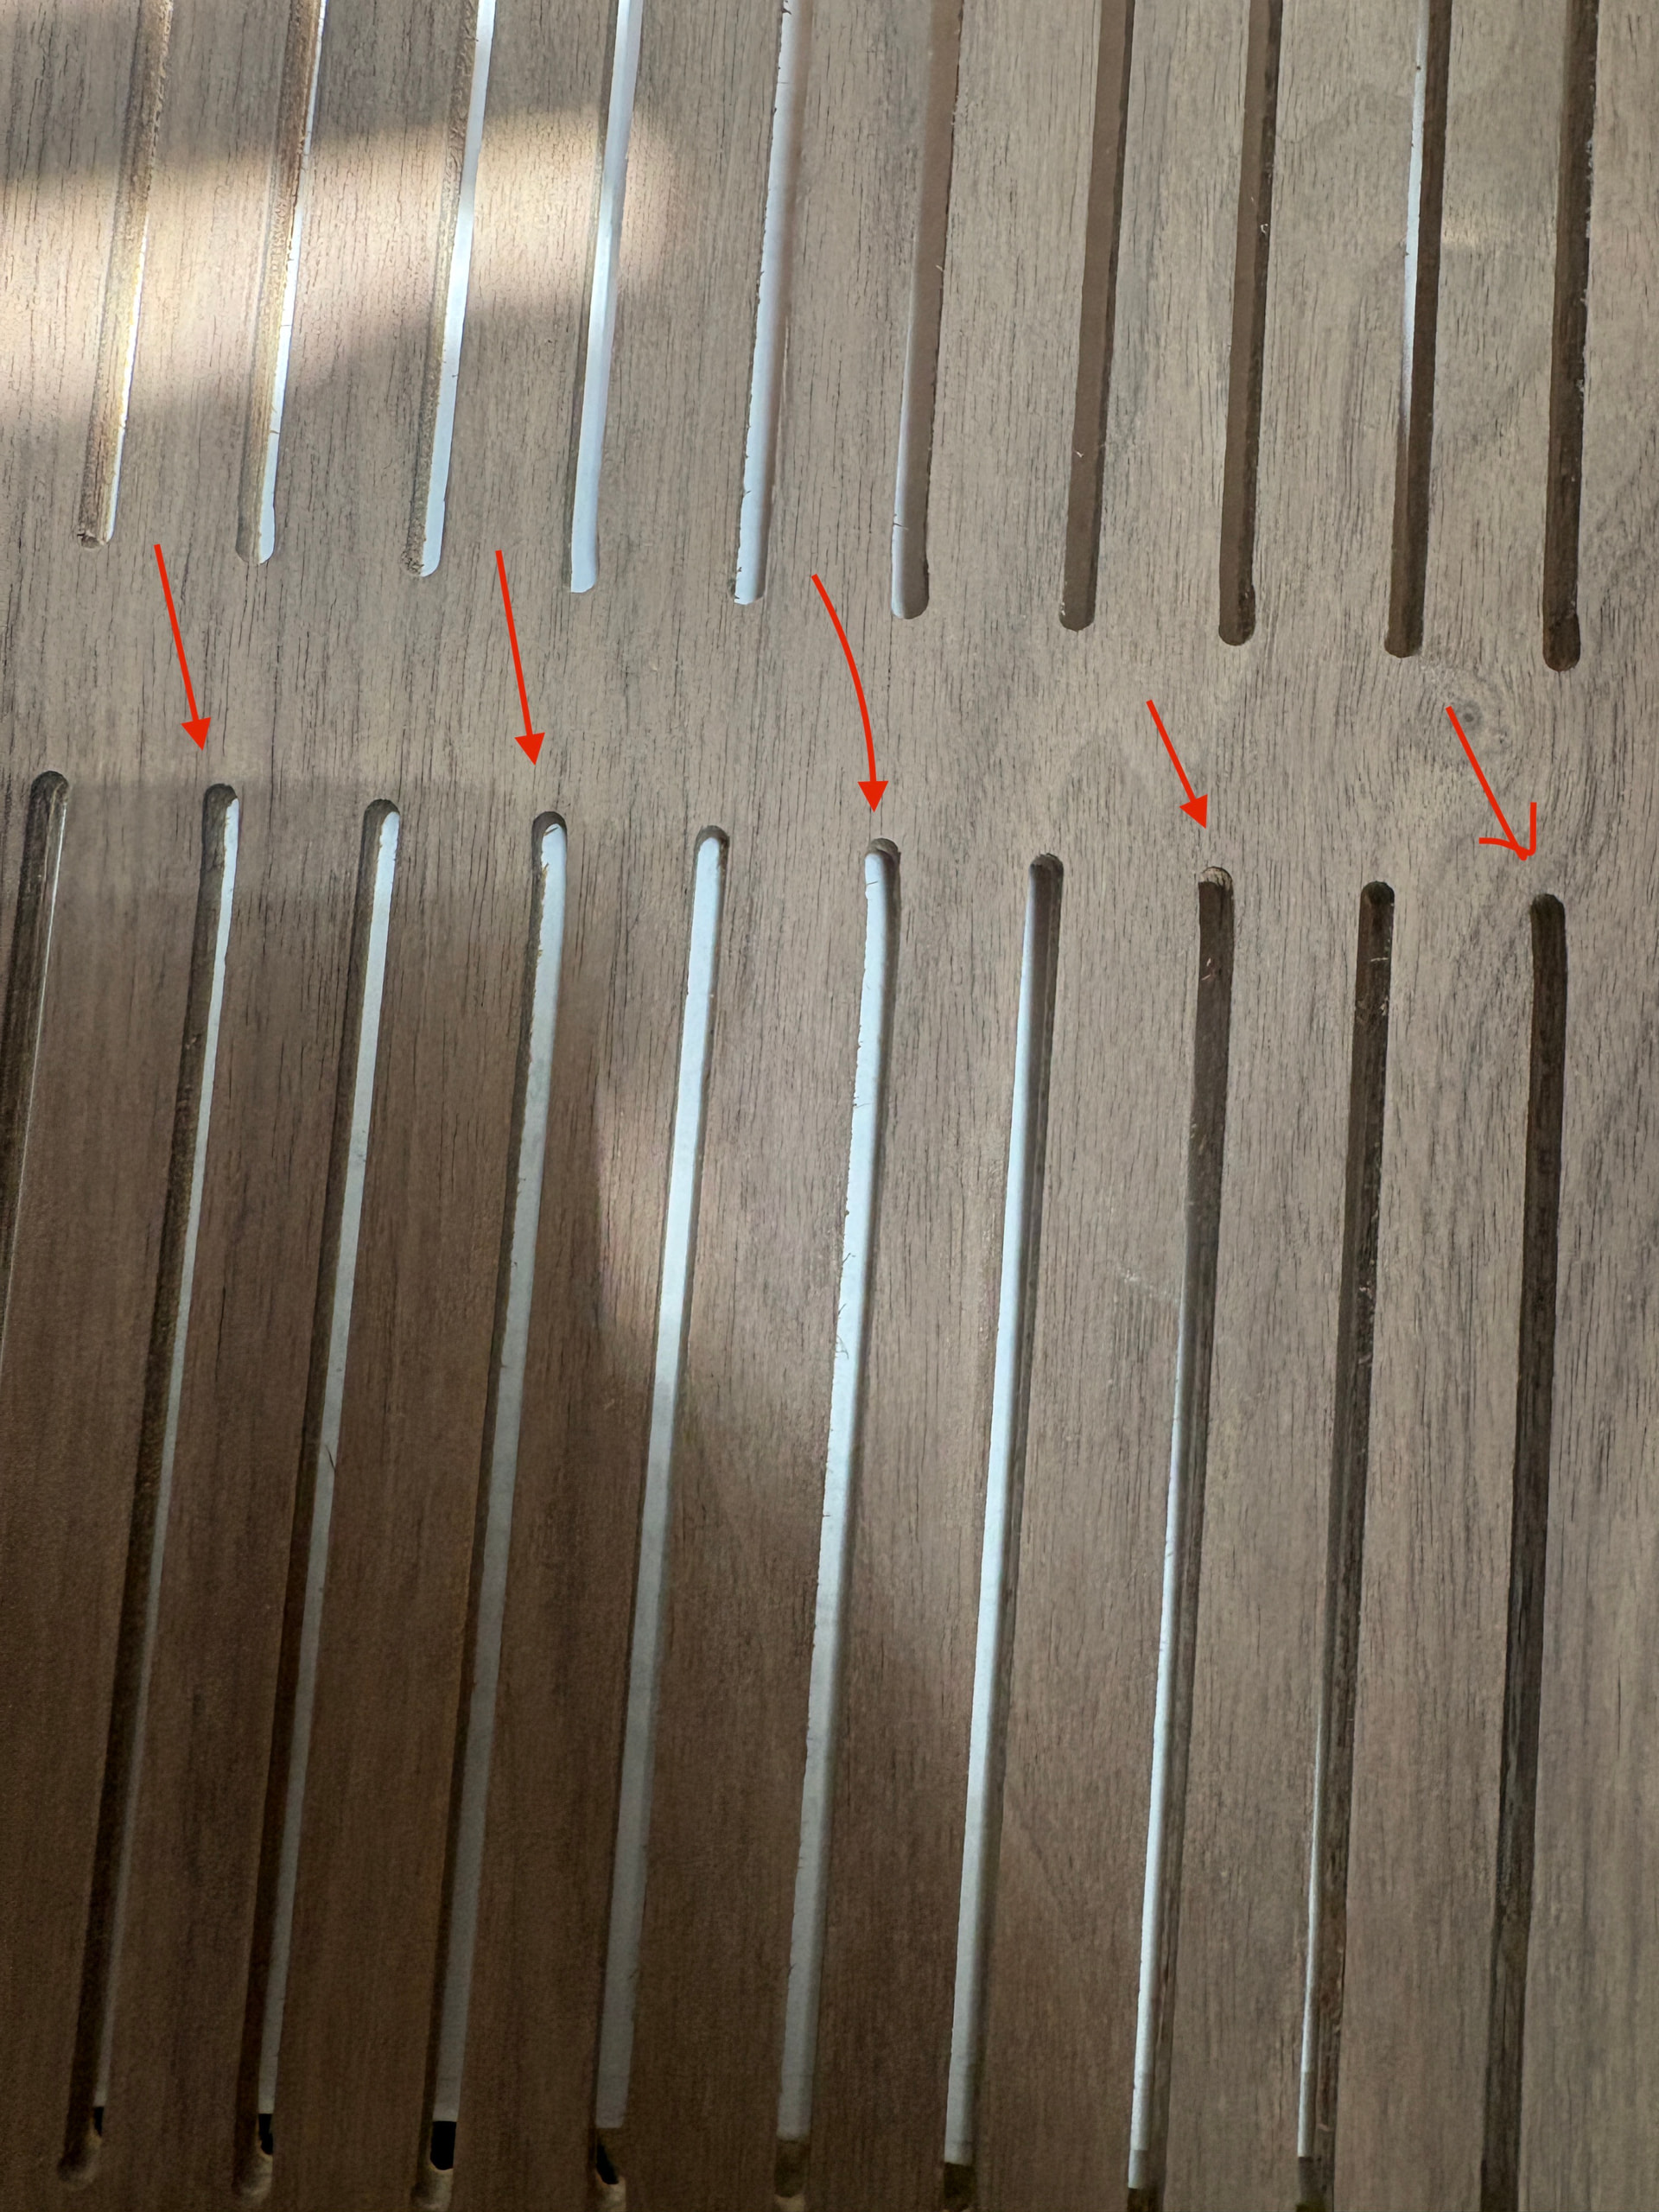
If those are full width slots you need pretty perfect feeds and speeds.
It might be easier to use wider slots or a more narrow endmill to let you use a full depth finishing pass all the way around.
It is odd that the ends all have something wonky about them. Is that the starting end or the finishing end?
I believe those are the the finishing end… can’t remember how Millmage handled the path, will double check. Yes, those are 1/8 grooves for 1/8 inch endmill… live and learn! I’ll redesign for a mm or two wider and even them up.
What is really crazy is the perfect skipping a row. One perfect, one wonky, etc. I could understand uniform but that’s got me puzzled.
Will tighten belts and back at it.
It must be changing direction, up and back, the other end being funky??
Yeah that should fix it.
Yeah, you can see it in the top rows, there every second bottom is off. Seems to have to do with climb vs conventional?
I believe that is it… entry point vs exit I am at work but snuck a look at my phone with a video and they do alternate… goes L to R, then R to L, etc on each pass. Now just need to determine if entry or exit are wonky. They are there for cooling so larger slots will only allow more heat to pass through so all good with larger slots within reason. So a few more passes will not be a bad thing.
Looks like each spot that messed up is the end of the cut.
I’d just leave it like that. It’s one of the earlier projects, they don’t have to be perfect and you’ll always remember them. 
Wise words. I may do just that
Very much so either a pocket or a cutout wit a 1mm or 2mm mill  or a 4 mm slot and pocket
And if you have someone looking that critically send them home without desert 

I was unable to design for the pocket in Millmage (new to all of this) and could not figure out the offset to turn a 3mm line into a 4mm pocket… tested it in cutting foam and my design was either bit width or too fat so I regrouped and decided “good enough” ! Did not have the guts to run the part again when it was so close to how I intended it. I have learned a whole lot on this project and will be ready to go for next one… I have some more projects to do in the near future.