Finally had a weekend with time to work on some upgrades for my LR4.
I was planning on on finally cleaning up the wiring and adding router control from my jackpot. Got pretty close on that one but I’ll come back to it.
I also planned on reprinting my core. I suspect that my current core (printed out of PLA) may have deformed over the summer in my garage here in extreme southwest AZ. I was still able to successfully cut foam on the machine in Sept but noticed the core was loose on the rails despite tightening up the adjuster screws. I had actually noticed quite a bit loose on the machine even earlier - but most of it was just screws I suspect I may never have gone back and fully tightened after initial assembly.
So I decided to bite the bullet and redo my core (and possibly a few other bits) in PET-CF. I ordered some Siraya PET-CF and it’s been sitting here for a few weeks as I worked up the nerve and prepped my machine. My old homemade 3d printer I had upgraded to an all metal hot end and done quite a bit of printing in various Nylons - but since getting my Prusa Mk3 (later upgraded with MMU2 and to a Mk3s. I had also bought a Nozzle X hardened nozzle when they first came out but the Prusa just worked so much better than my old printer I never bothered to install the Nozzle X as I never got around to any material that would justify it. But honestly after 8 years of use I was suspecting my nozzle was ready to be replaced anyway. So I dusted off the X and finally installed it this week.
Confirmed things were printing well with PLA still and then started prepping for trying the PET-CF. Did a PID calibration a 295 - but hit MAXTEMP. Tried again at 285 and it went well, so then did a thermal model calibration. Seemed alright…Tried printing a little test piece for my wife’s son’s RC car and twice in a row got about 6mm off the build plate and hit MAXTEMP printing at 295. Ok…too close to the MK3’s 300c max. Dialed back to 290 and tried again…success! Part looks great, even better than the one I did a week ago in PETG with my old nozzle.
So..bit the bullet and tried the core at 290. I’m running really slow at 0.20mm layers and a 0.4mm nozzle with max volumetric flow throttled to just 6mm3/s to make sure my hot end and 0.4mm nozzle can keep up. 42 hour print. Ugh…but I’ve got nothing better to do so let’s go for it - will be worth it if it works.
And it almost did.
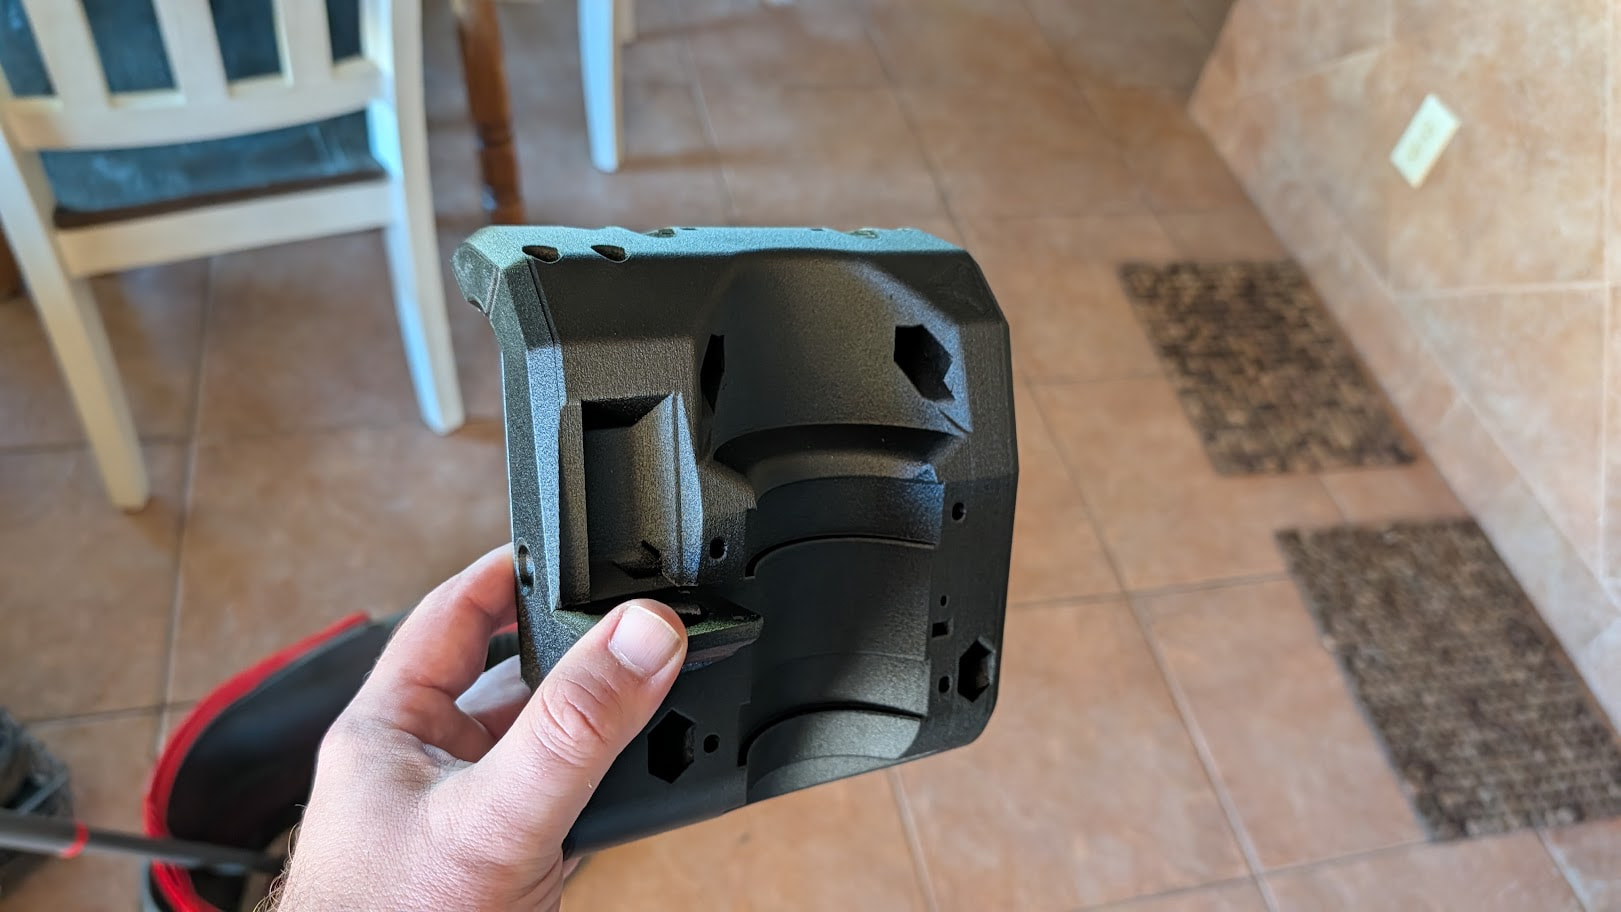
Except 30 minutes before it finished it hit MAXTEMP and shut down again 
Ugh. It’s just a few final outer layers on one side, and the print look gorgeous at first glance…I started thinking about maybe just trying it…but then I noticed 2 bigger issues.
First the other side has a BUNCH of zits…and they are SHARP. Could probably clean them off ok though…I assume they’re because I ran very little retraction as I was warned PET-CF doesn’t do well with retraction. Not the end of the world…The other problem though:
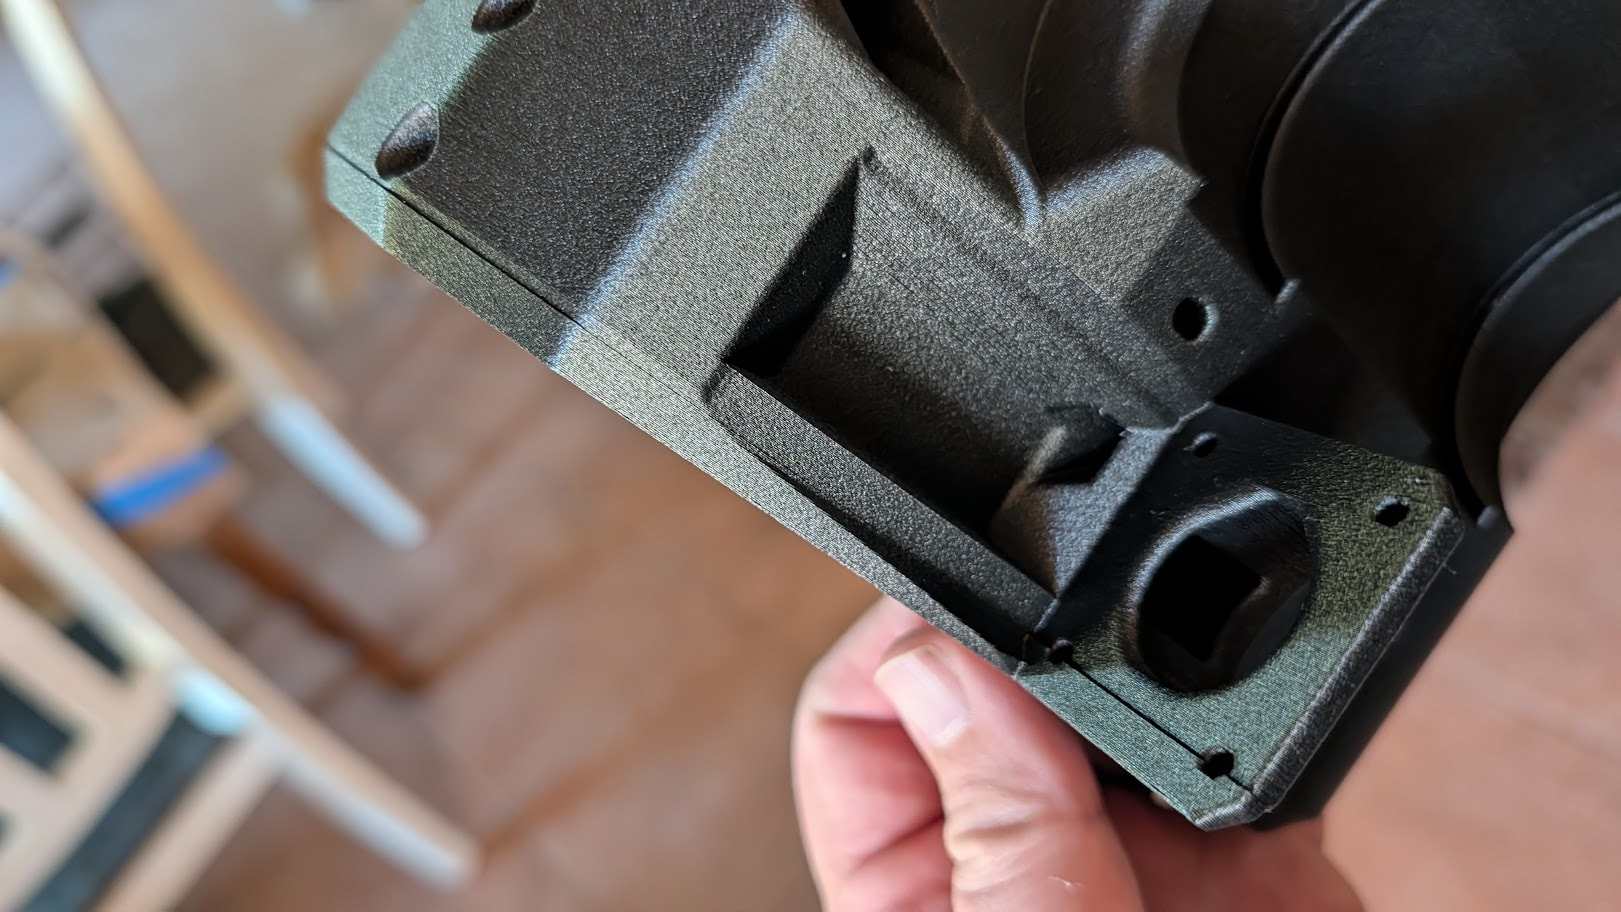
Well, shoot. I had a layer shift right at the start of the print that I never noticed. My printer is in an enclosure with fairly poor light and I’ve got a bunch of boxes in front of it so I kind of have to lean over to even get to it right now. So even though I had checked on the print regularly I totally missed it
And the part weights 527g so I almost certainly don’t have enough left on this 1kg spool to do another try.
I’ll probably print the tool mounts and maybe some braces the next few days to get a better feel for the PET-CF while I wait for a new spool to try again on the core. Just so frustrating to have a print go great for 41 hours then fail in the last 30 minutes.
The other upgrade is going better…but hasn’t made it to the machine yet.
I already shared some of this in @jeyeager’s amazing sandbox post. Short version to catch everyone up…I was playing around with claude and the Fusion MCP and ideas to clean up some of my wiring and let the jackpot control power to my router. You can see the renderings in the linked post…but the meanwell DIN rail power supply I had been waiting on finally arrived and I was able to start wiring things up:
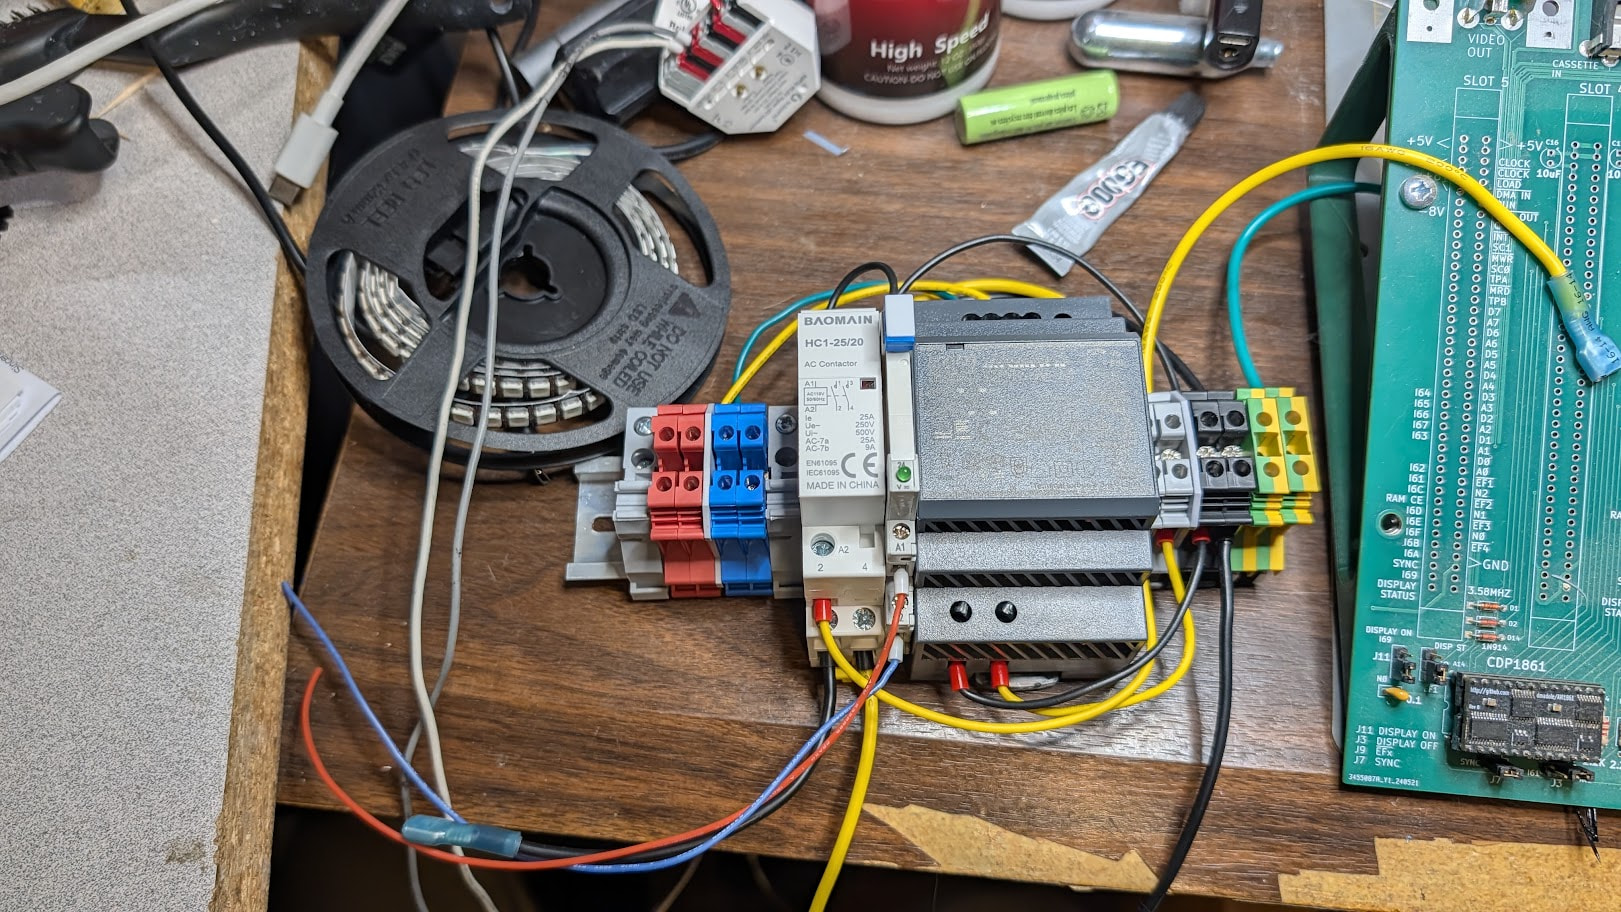
(That’s also a roll over WS2812B’s and a little WLED controller - claude helped me update @jeyeager’s usermod to the new format and build it against the latest WLED…I haven’t actually tested the usermod itself yet. Will share a PR with the changes if it does work when I finally get around to testing it.)
I also printed the case Claude designed and it fits…but had to hit three local stores to find the right length 4m screws to mount the DIN rail:
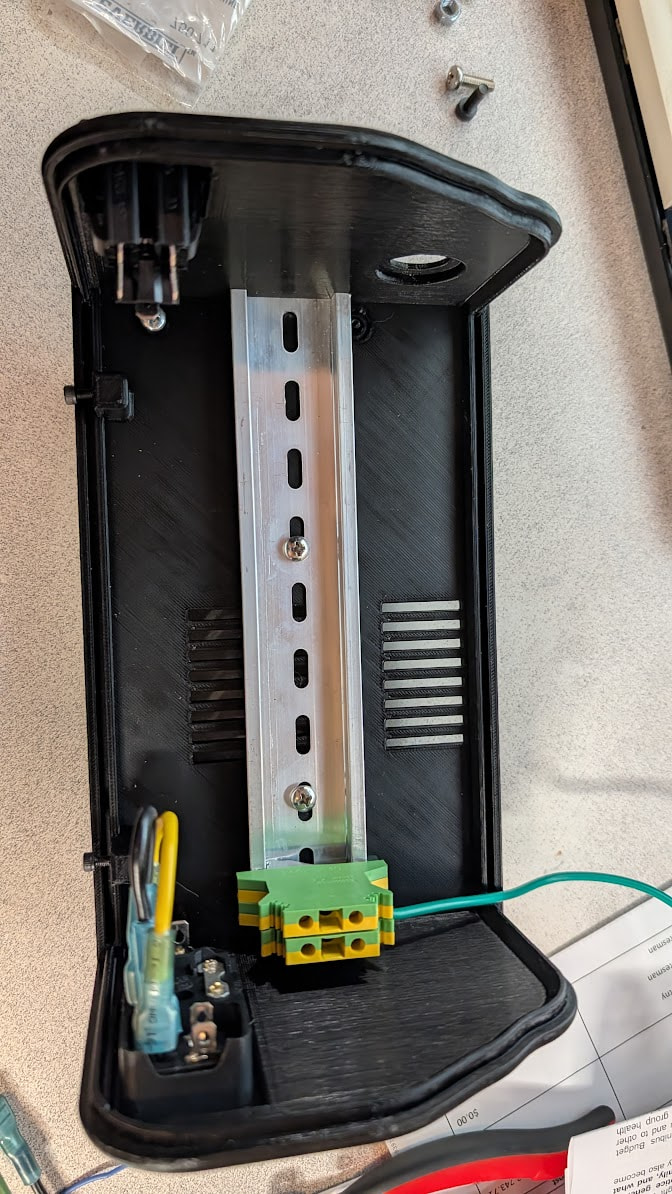
It IS fully wired now and fits in the box. I just apparently forgot to take a photo…and haven’t double checked everything or tried putting power to it just yet. I’ll still have to mount it to the plate on my LR4 and make the final wiring harness between it and the Jackpot.
Oh well, at least the weather is finally getting nice enough I can spend time out in the garage without running the garage AC so hopefully progress will go better.

