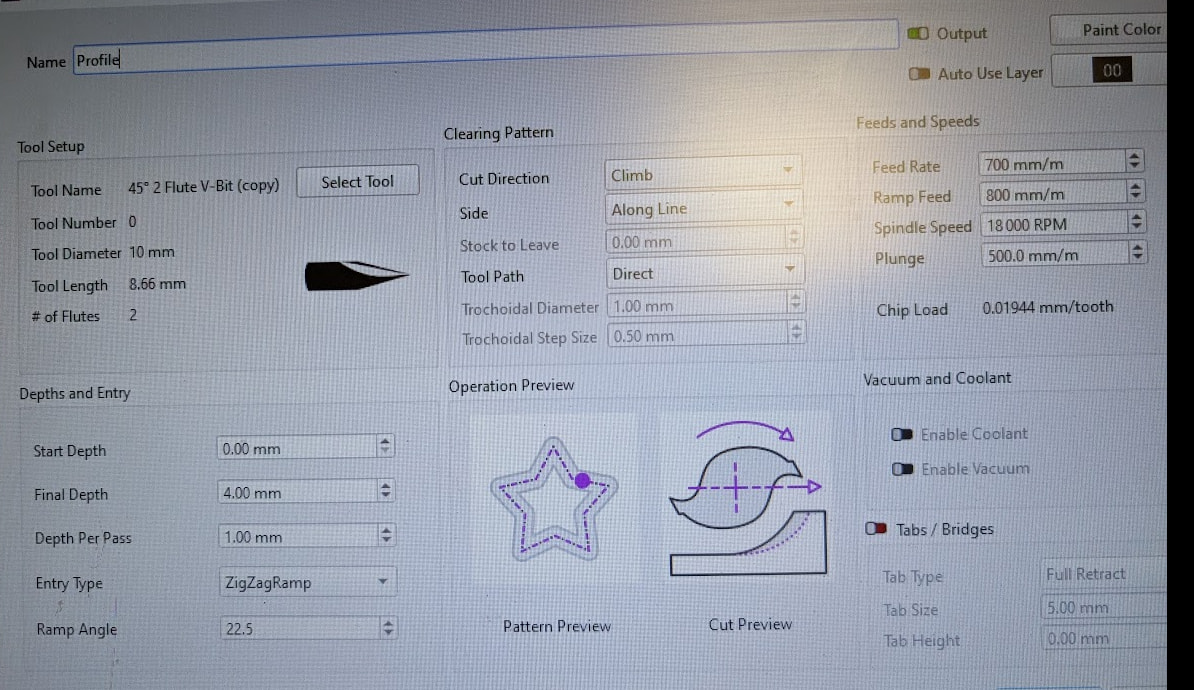
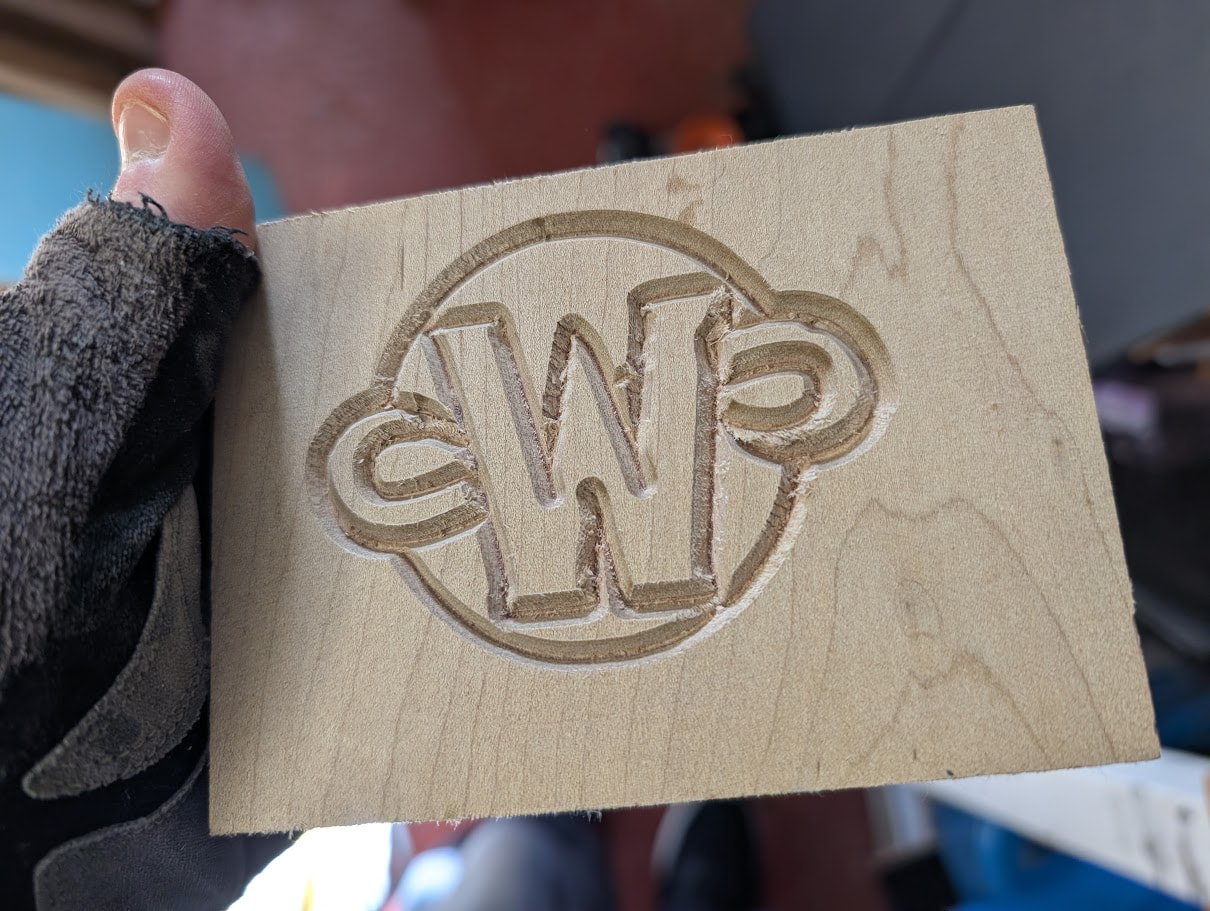
So just resurrected my MPCNC this past week and so happy to have it up and running again, after bit of toying around, getting used to MillMage (damn it’s so easy to use - definitely on Santa’s list)
But some quality issue here with rough edges…I was wondering for quick bit of Feed speed advice here, doing a v carve on a makita clone router running on speed setting of 5 or 6 and these settings below, default was higher so did drop it but wondering what feeds I should run at and if router speed should be slower or higher end to not has a rough walls ?
Also need to check if it was the logo or my belts need tightening up etc as lines look bit wobbly in places so not sure there till I go back in the workshgop
Recommendations on a proper spindle that can be controlled by the SKR Pro 1.2 ? UK Based, also where’s best to get bits UK wise that have feed and speed sheets to go along with what you buy rather than 10% guess