Hi everyone,
I built a Lowrider over the past few months and did already a few cuts. I have no table yet and still sort out a few things but the results are already pretty solid if I don’t cut to aggressive.
After lurking around here for almost a year I wanted to join the community and share some feedback and ask some questions.
So the machine is currently on top of 3 C-grade plywood sheets with another one as spoil board.
I wanted to cut the frame for the torsion box table out of that but I think I’ll get a MDF one and use two of the other sheets as top and bottom plates. On the left you can see some beams I want to use for the legs.
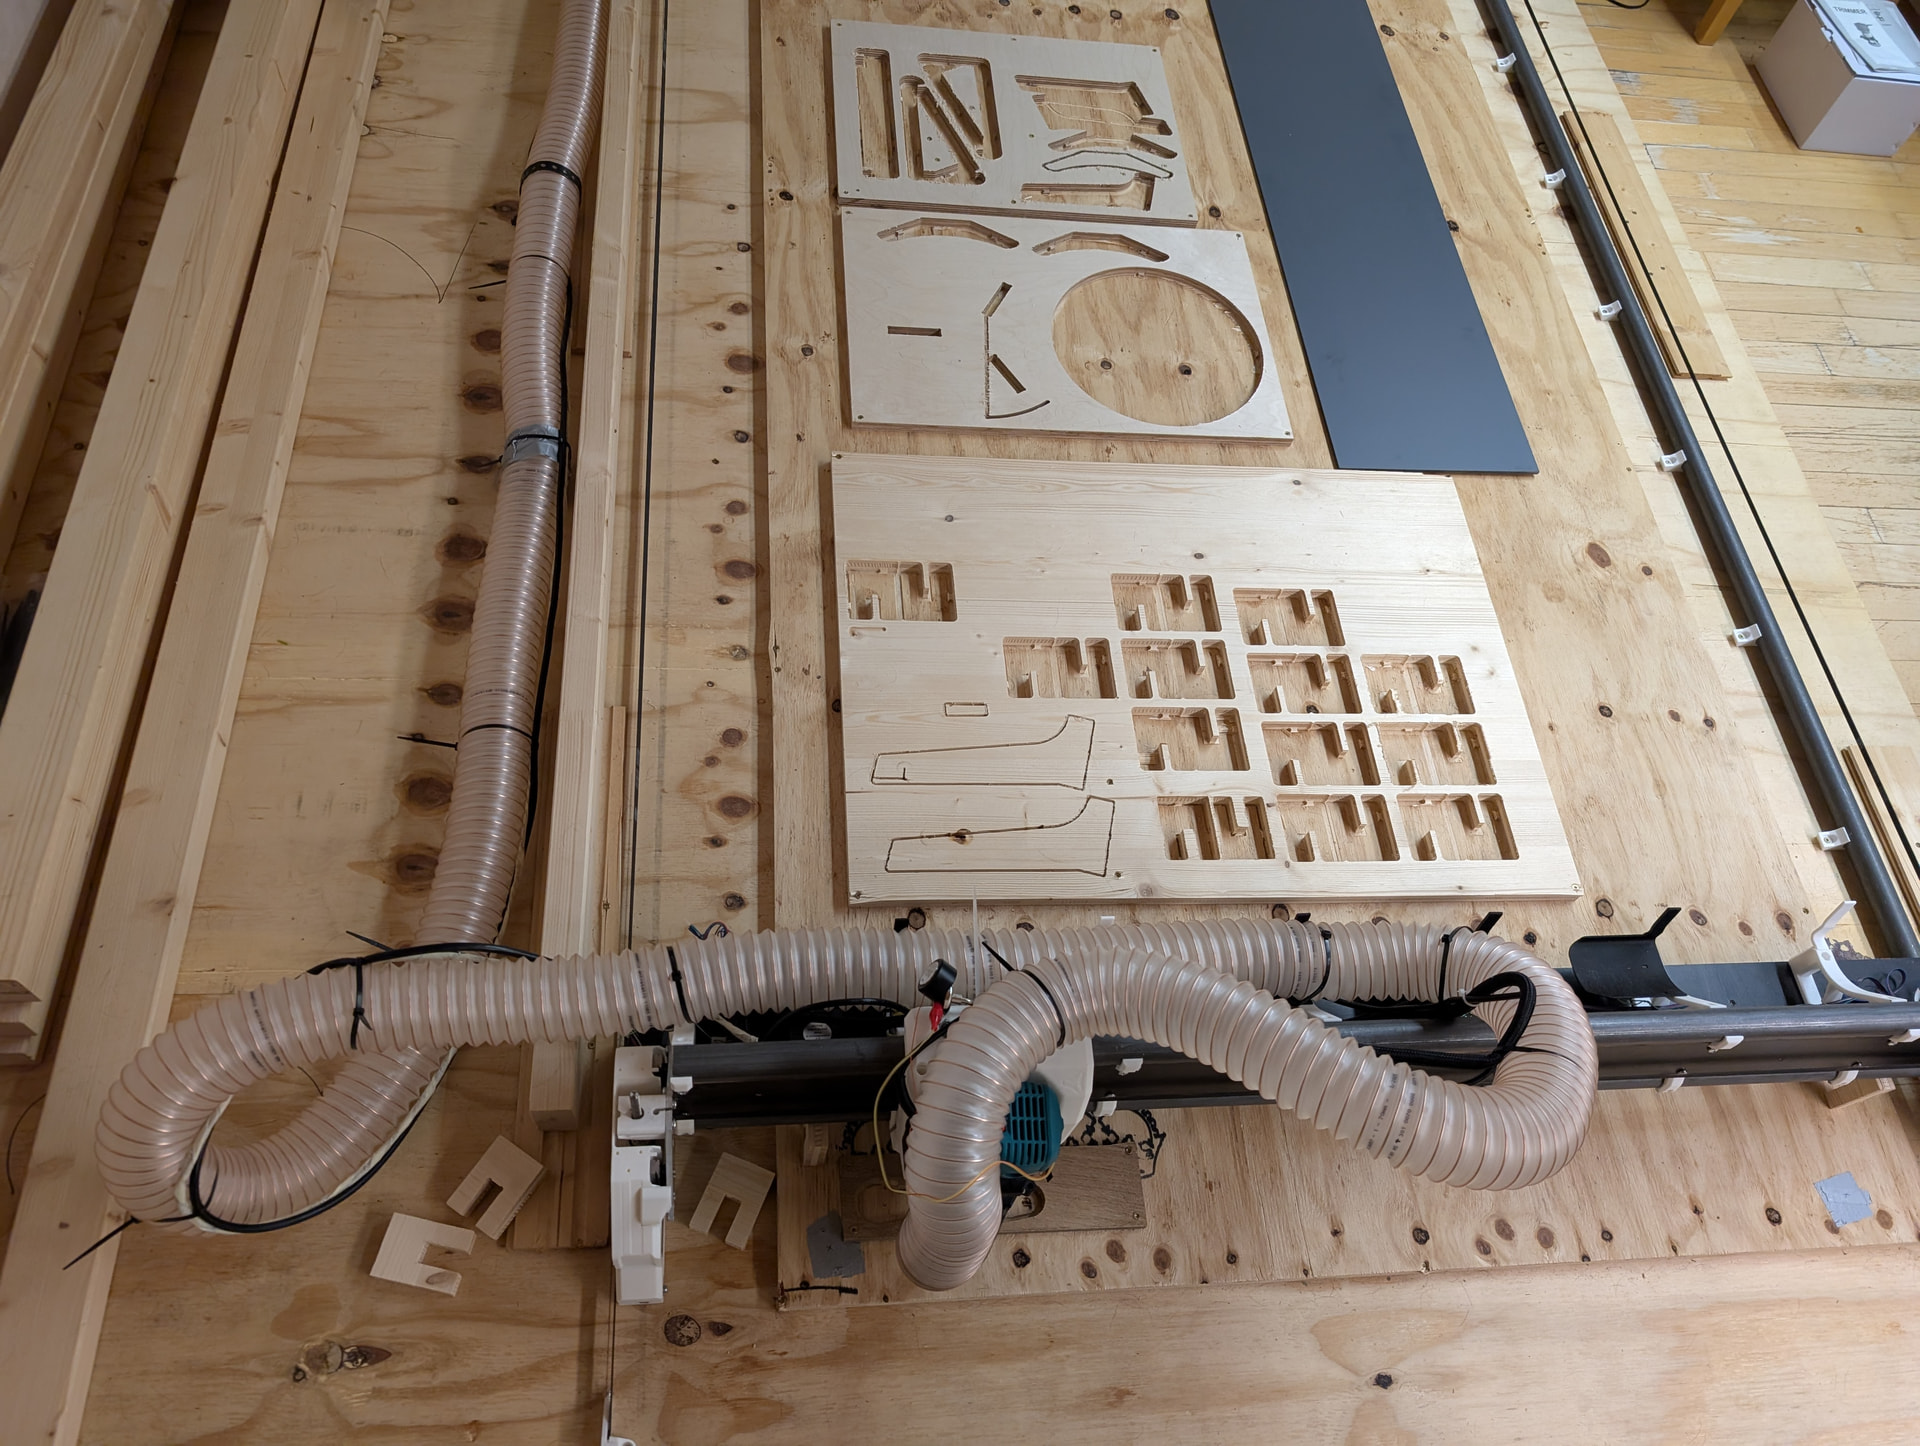
If you look close you can already see some spots where things got wrong. But I managed to build the plant stool and laptop stand from ZenziWerken with an OK quality. Also I did a lot of test cuts to get a better understanding of the machine. These are the test parts from @franklyrosalind torsion box table generator which I want to use for the table later.
I started planning the build around November last year, the general key attributes are:
- Full sheet (2500mm x 1250mm)
- Jackpot 1 controller
- Makita clone router
- Self-sourced, Alu plates from @Tokoloshe

- My brother-in-law printed the 3D parts for me, most is PLA except for the braces on the router and I think the jackpot box, these are made of some carbon reinforced stuff
- vac with cyclone separator (this works insanely well)
So generally speaking it is an awesome machine Ryan, very nice work!
I had quite some struggle but I might have created an account earlier to get some help.
Here some feedback/problems, maybe it helps others:
- The build took really long until I managed to cut the first parts, there were some unlucky circumstances for example where I had to move the machine but I also had several times some weeks a break. I do not recommend this, it costs extra time to get back into it.
- Finding all the parts. I didnt want to import from US because the shipping is pretty expensive and Philipp didn’t had the full set back then. I really strongly recommend buying the set if possible, I spend way to much time getting all the parts
- Follow the ‘yellow brick road’. It is so motivating to get the machine running so try to keep it as simple as possible first. I did build the pendant but don’t use it currently, so I’d better have focussed on the machine itself
- Language - while my english is pretty solid there are still alot of special terms and parts in the CNC world which I needed to learn, so thats an additional challenge
- Core wiggle, I did tighten the core like 3 times (yes wtf) maybe I was overly carefully at the beginning
- without strut plates it was a mess. My strut plates are right now 4mm phenolic plywood (idk if thats the right translation, we say Siebdruckplatte in german) when I cut them the DoC was partially deeper because the surface is everything but flat and the force was so big that the whole XY plates would just get pulled to the center a few mm until the x-belt tension would get to low. On the other hand the Y trigger on Y0 would just drive past the screw instead of triggering. with the struc plates the gantry has the correct width now. But the strut plates are still pretty flexible so I bought a plate of 6mm HPL for new ones (the black plate in the picture)
- after I moved the machine and reassembled it I did some calibration again and interestingly the value for the belt step length changed a bit. Like from 50.124 to 50.07 or so. Did anyone do the calibration as well after a while and had to change it?
- I bought some thread locker, the red one instead of the blue, so might be worth adding an hint that you should use the blue one to the docs
- the vac hose was to short. I just ordered 3m (how should that be enought for a full-size build lol?) So I ordered another 2m. Generally speaking it was quite a challenge to get into the whole topic and there is some info missing like that, it might help to have the values for atleast the standard sizes (full- / half- / quarter-sheet). I had for example to search for the required length of the endstop cables since I had really no clue. I found it under a video of aza I think. But I was pretty overwhelmed of the many topics so this info would maybe also be a nice addition.
- The x-stepper plug would go off sometimes. Somewhere I found the tip with the drop of hot glue, very nice might also be a candidate for docs
- The docs are generally very good, I really don’t want to complain
- I tested 2-flute 1/8" upcut and 2-flute 6mm compression and now mostly use 6mm 1-flute upcut now. I do unterstand it now better why to use the 1-flute but should simply have sticked to the recommendations. Also the compression one is to long (32mm blade) There is so many details you are not aware of if you are new to the cnc topic…
- Do you think it’s worth to get some 1/8" 1-flute upcuts or are the 6mm ones fine? I have read the deflection is much higher on the narrow ones.
- my router is a cheap 60€ makita clone and I planned from the very beginning to replace it when I know what I need. So at least not to much money burned. But I mostly run it on 3 / 6 (22RPM) because lower it has pretty low torque. Maybe I will buy a AMB I’ve heard it is good?
- I was losing some Z0 steps so I cleaned the leadscrew and lubed it, I also increased force by 0.1 amps, no more problems so far. But I also got aware I need to pay attention to the vac house there. When I have the table I want to find a better solution there.
Sorry for the wall of text, there is many more details and I think I will just add it when it comes to my mind, but at least I did open the topic for now…
So nice to meet you
Jannis