Im still unsure if what I have is the same issue as Michael on his last post.
After some time cutting with no issue I started having problems today again.
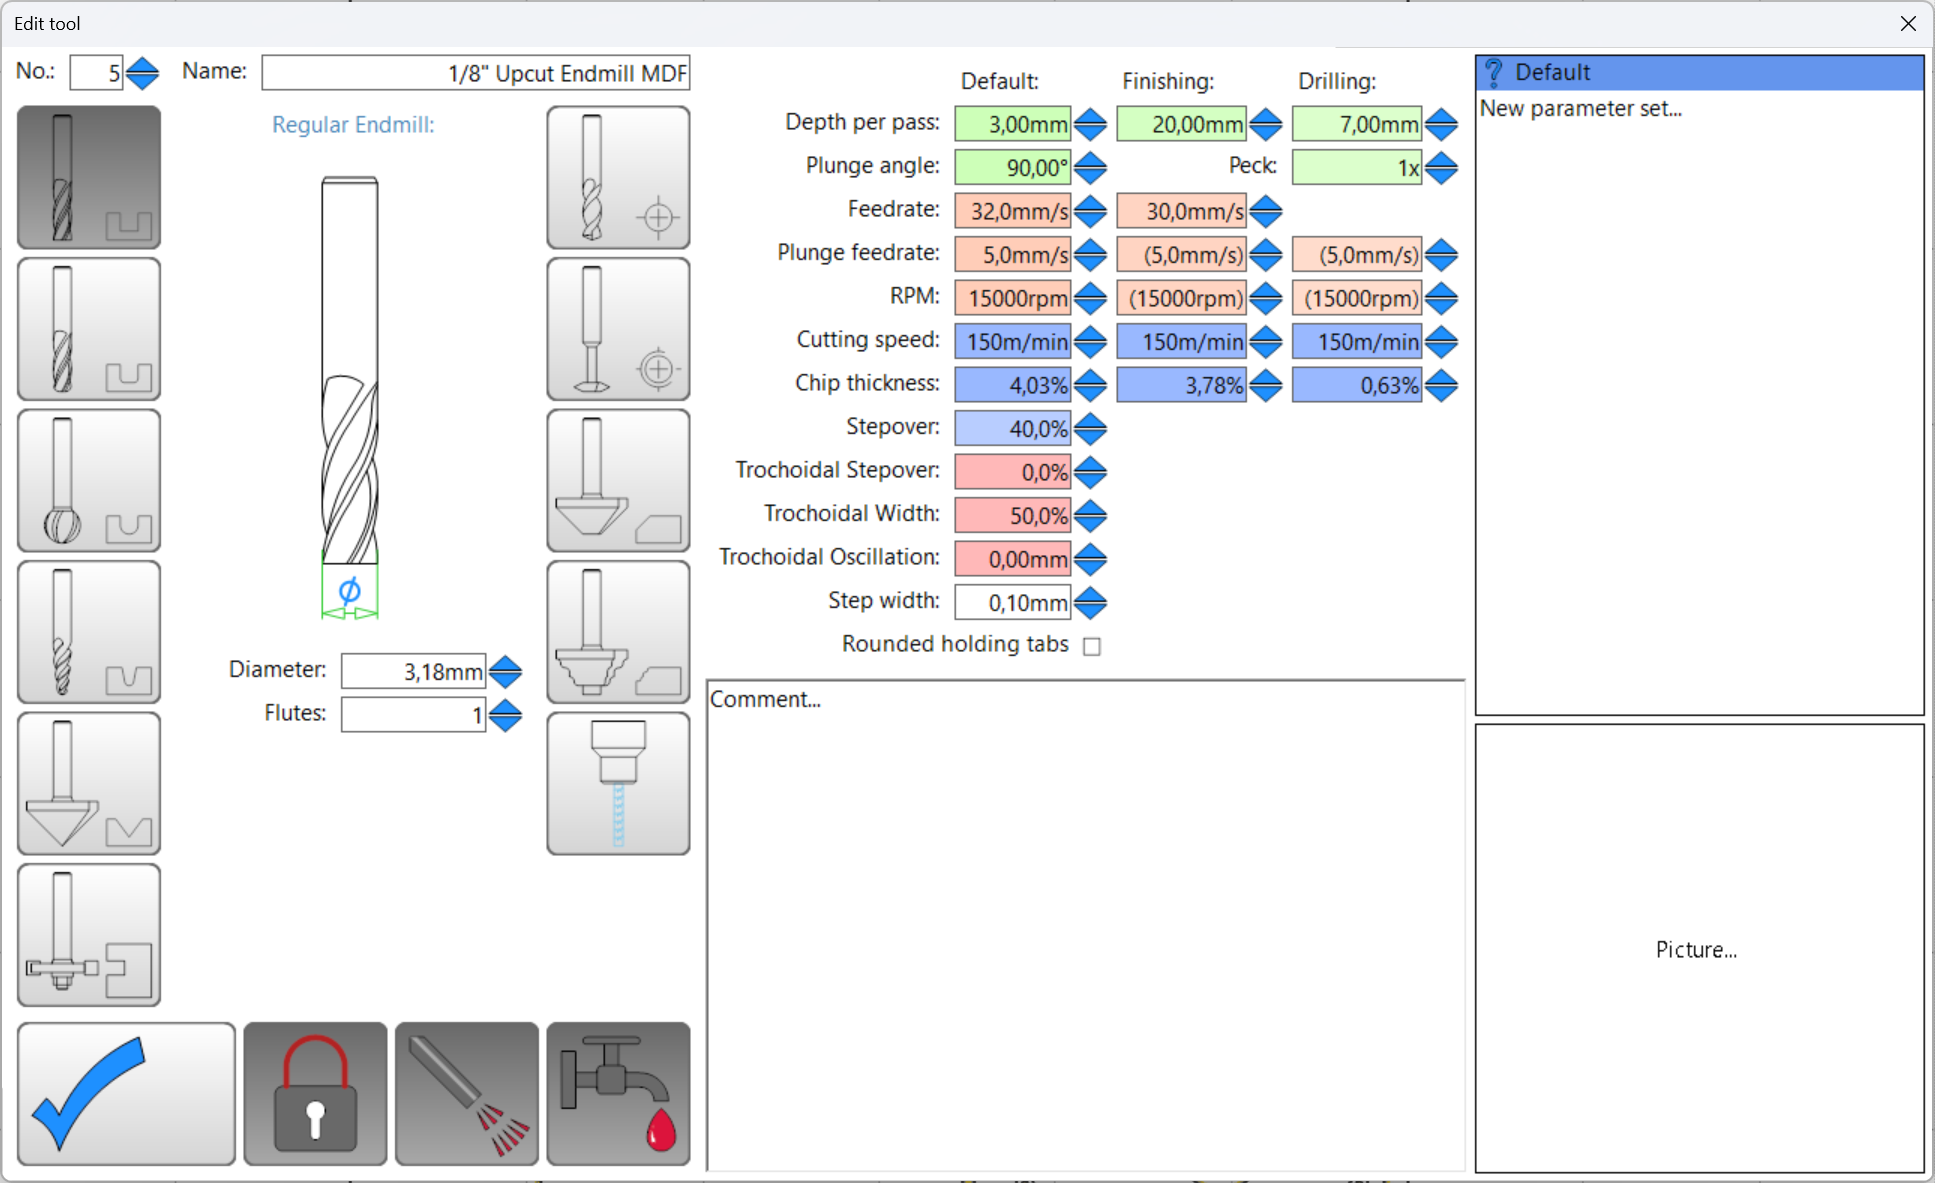
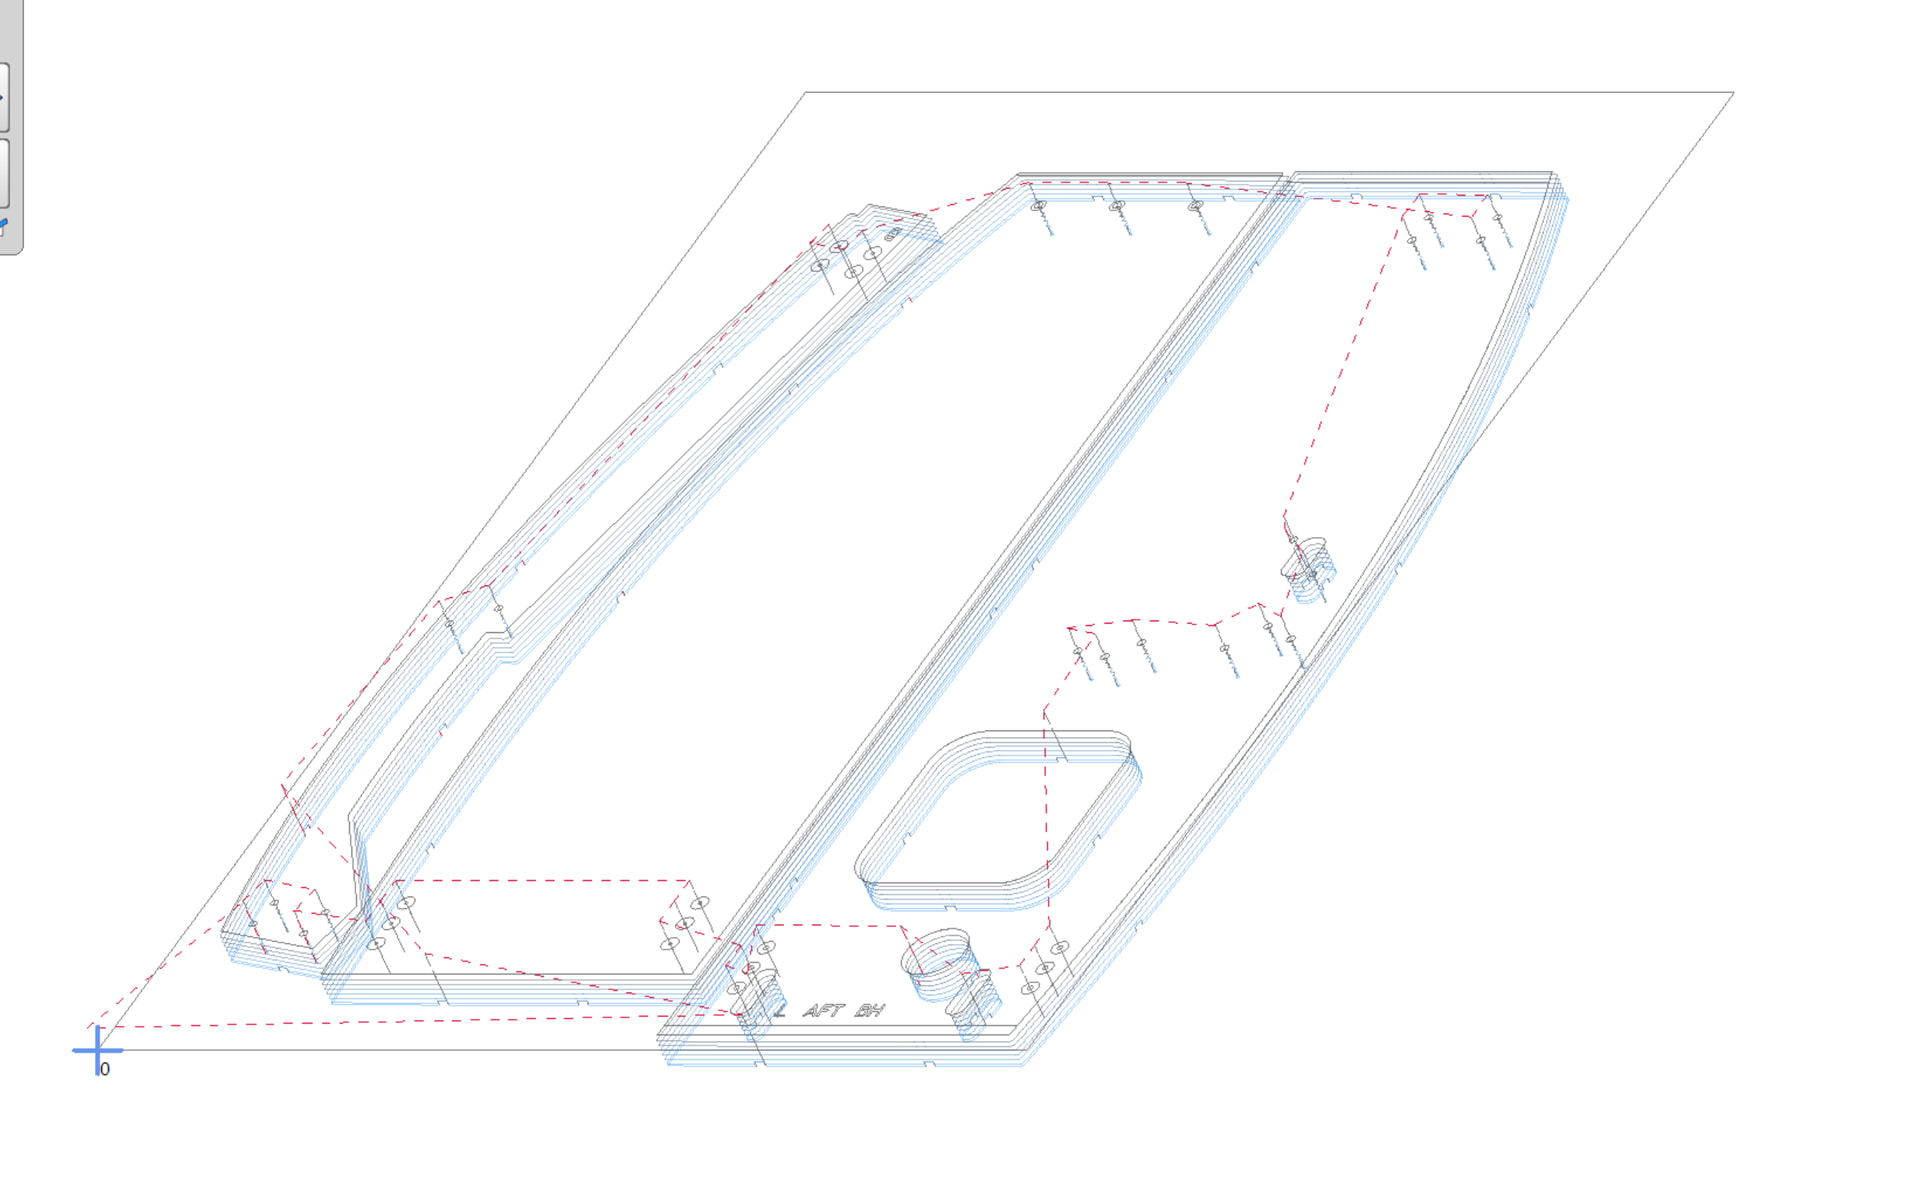
And the issue is that I started noticing that the machine seemed to be plunging more than it should. The reason why I noticed is because I started cutting a full sheet of 19mm MDF with several pieces on it. Normally with my settings it takes 7 passes to complete each piece. My router bit is 1/8 inch and depth per pass is set to 3mm.
All of them had 3mm tabs, which always has been more than enough to keep the pieces in place. This means that normally the tabs get done in the pass 6 and 7.
But the first pieces that were cut started to become loose even before I reached passes 6 and 7.
So I noticed that the machine was reaching the end of the MDF in less passes than usual. In fact in one of my last pieces by the time it reached pass 7 it was cutting into the wasteboard and the collet had reached the top of the working board and was rubbing on it so I had to stop the work.
This started happening today
I checked that the bit wasnt becoming loose. I still have the same settings ive been using to cut several sheets, which are very conservative and that Ive been using since my last issues cause they havent given me any problem with overheating.
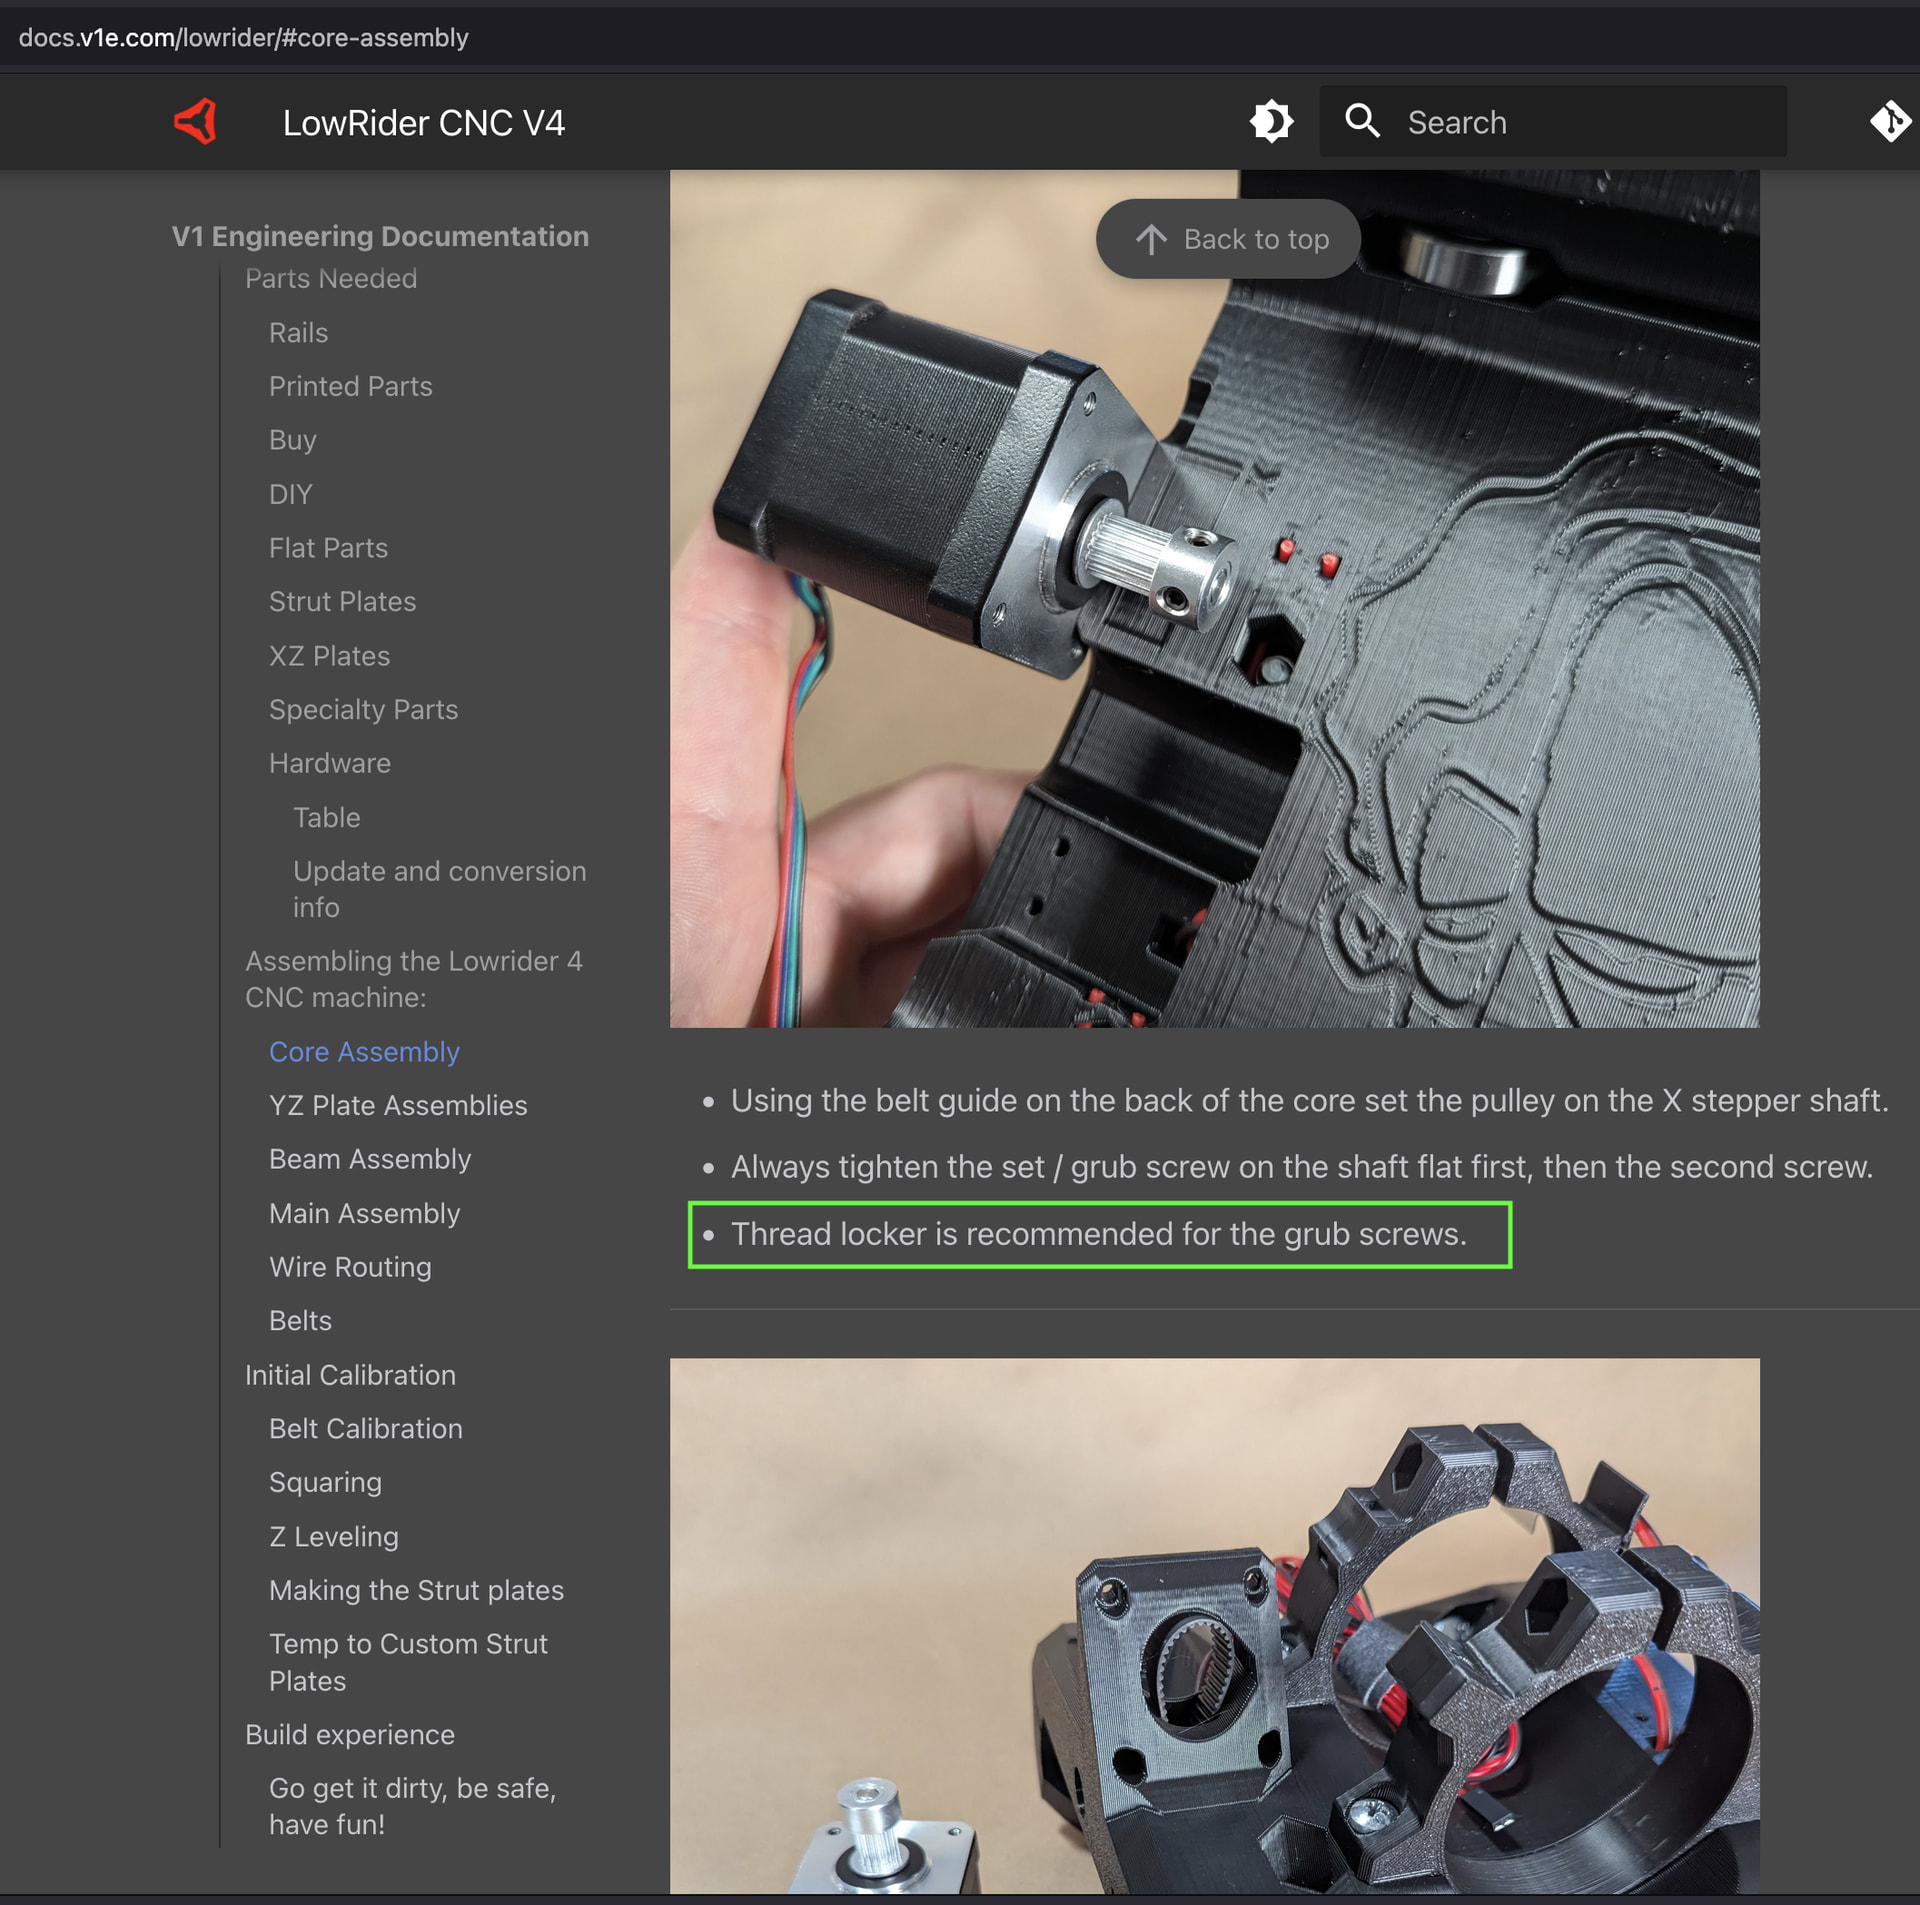
At this point Im wondering if the grub screws of the Z axes have become loose or something
With regards to the grub screws I dont have yet the blue loctite on them. I bought it because I had some issues in the past with some other screws of the machine becoming loose. I actually suggested that maybe would be good to put the suggestion to use blue loctite on screws in the instructions of assembly. It doesnt cost a lot and doesnt interfere with anything and avoids possible problems in the long run
As sson as I can I will check the state of the screws, tighten them and apply loctite to discard that problem (havent had time as I arrive quite late home)
So I checked today and didnt seem like the grub screws were loose. I can reach the ones that hold the main z axes screws but not the ones that attach the couplers to the steppers without having to dismantle everything
I tried a calibration on z and it was still less than 1 mm difference
I tried small cuts of simple pieces and the result was good so i dont understand what happened. The endmill didnt seem like it slip out either
This is unfortunately bad cause from prev experiences I know the problem is not gone and probably will come up again next time I try a full sheet
Ok so I did another attempt and it failed cause again it happened it cut to deep which meant the tabs that were supposed to be 3mm thick they were a lot thinner, so one of the holes became loose and the endmill got stuck on the piece cut from the hole so i had to stop completely the job.
So from this point I have several doubts:
For the x and z axis we have the mm per step that says how much the endmill advances per step of the belts,. but i dont see any option like that for the z axis. Is there a way to contrast how much the endmill is advancing in Z vs how much it thinks its advancing?
The other day I tried to do a Z level calibration. Figured out I need to add 0.6 mm to the pulloff of stepper 0 in Z. I went to the settings, set the setting from 4.0 to 4.6 and press save. As far as I know this should permanently save the setting in the flash. But as soon as I reset the CNC and I go to settings the pulloff is back to the original 4.0. The only way that I found I can do this is by getting the settings yaml, editing in in a text editor and then overwritiing the yaml in the machine. Am I doing something wrong?
Is there some sort of Z reset I need to do at the start of the cut? Im not sure what can have changed tbh. My process has always been the same. Turn on, home the machine, jog the endmill where I want my zero ref to be. Then start the job that will do first the Z probe process to know where the top of the surface is. So in theory it will go the depth I told him from the probed Z. The only think I can think about is that every time it does another pass and thinks its advancing on Z 3 mm is actually going down deeper
The things I can think about that could be happening:
When I probe Z i normally do at the front of the table. If the wasteboard is a little bit inclined up from the front to the back that means when i go cut things towards the back the machine is gonna go deeper in that side. I doubt this is the case cause the endmill has been milling into the wasteboard even at the front close to the probing point. When i do the Z level calibration do I need to measure at the 4 corners or just at 2 or how people normally do this?
The machine is plunging per pass more than 3 mm. (Its turning the screws more than it should)
The grub screws for the Z steppers are loose somewhere and im loosing steps
I can help with doubt #2 at least: there is a save button on the settings page but there is also a save macro button on the main page - I found that I needed to do both to get settings to survive a reboot. I think I saw this in the docs somewhere but it still tripped me up when I was first doing calibrations.