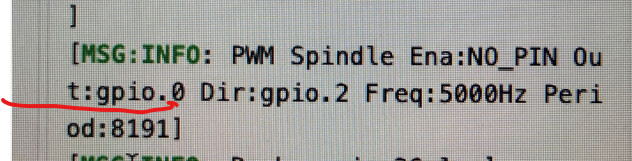
Using Jackpot3 and lightburn, laser does not turn off between layers (G0 moves). Does anyone have experience with resolving this? I have tried changing a few things in the config file, but no success. I also cannot change $32 to “1” in lightburn.
Thank you.
are you actually in laser mode in fluid nc ? how your spindle is configured
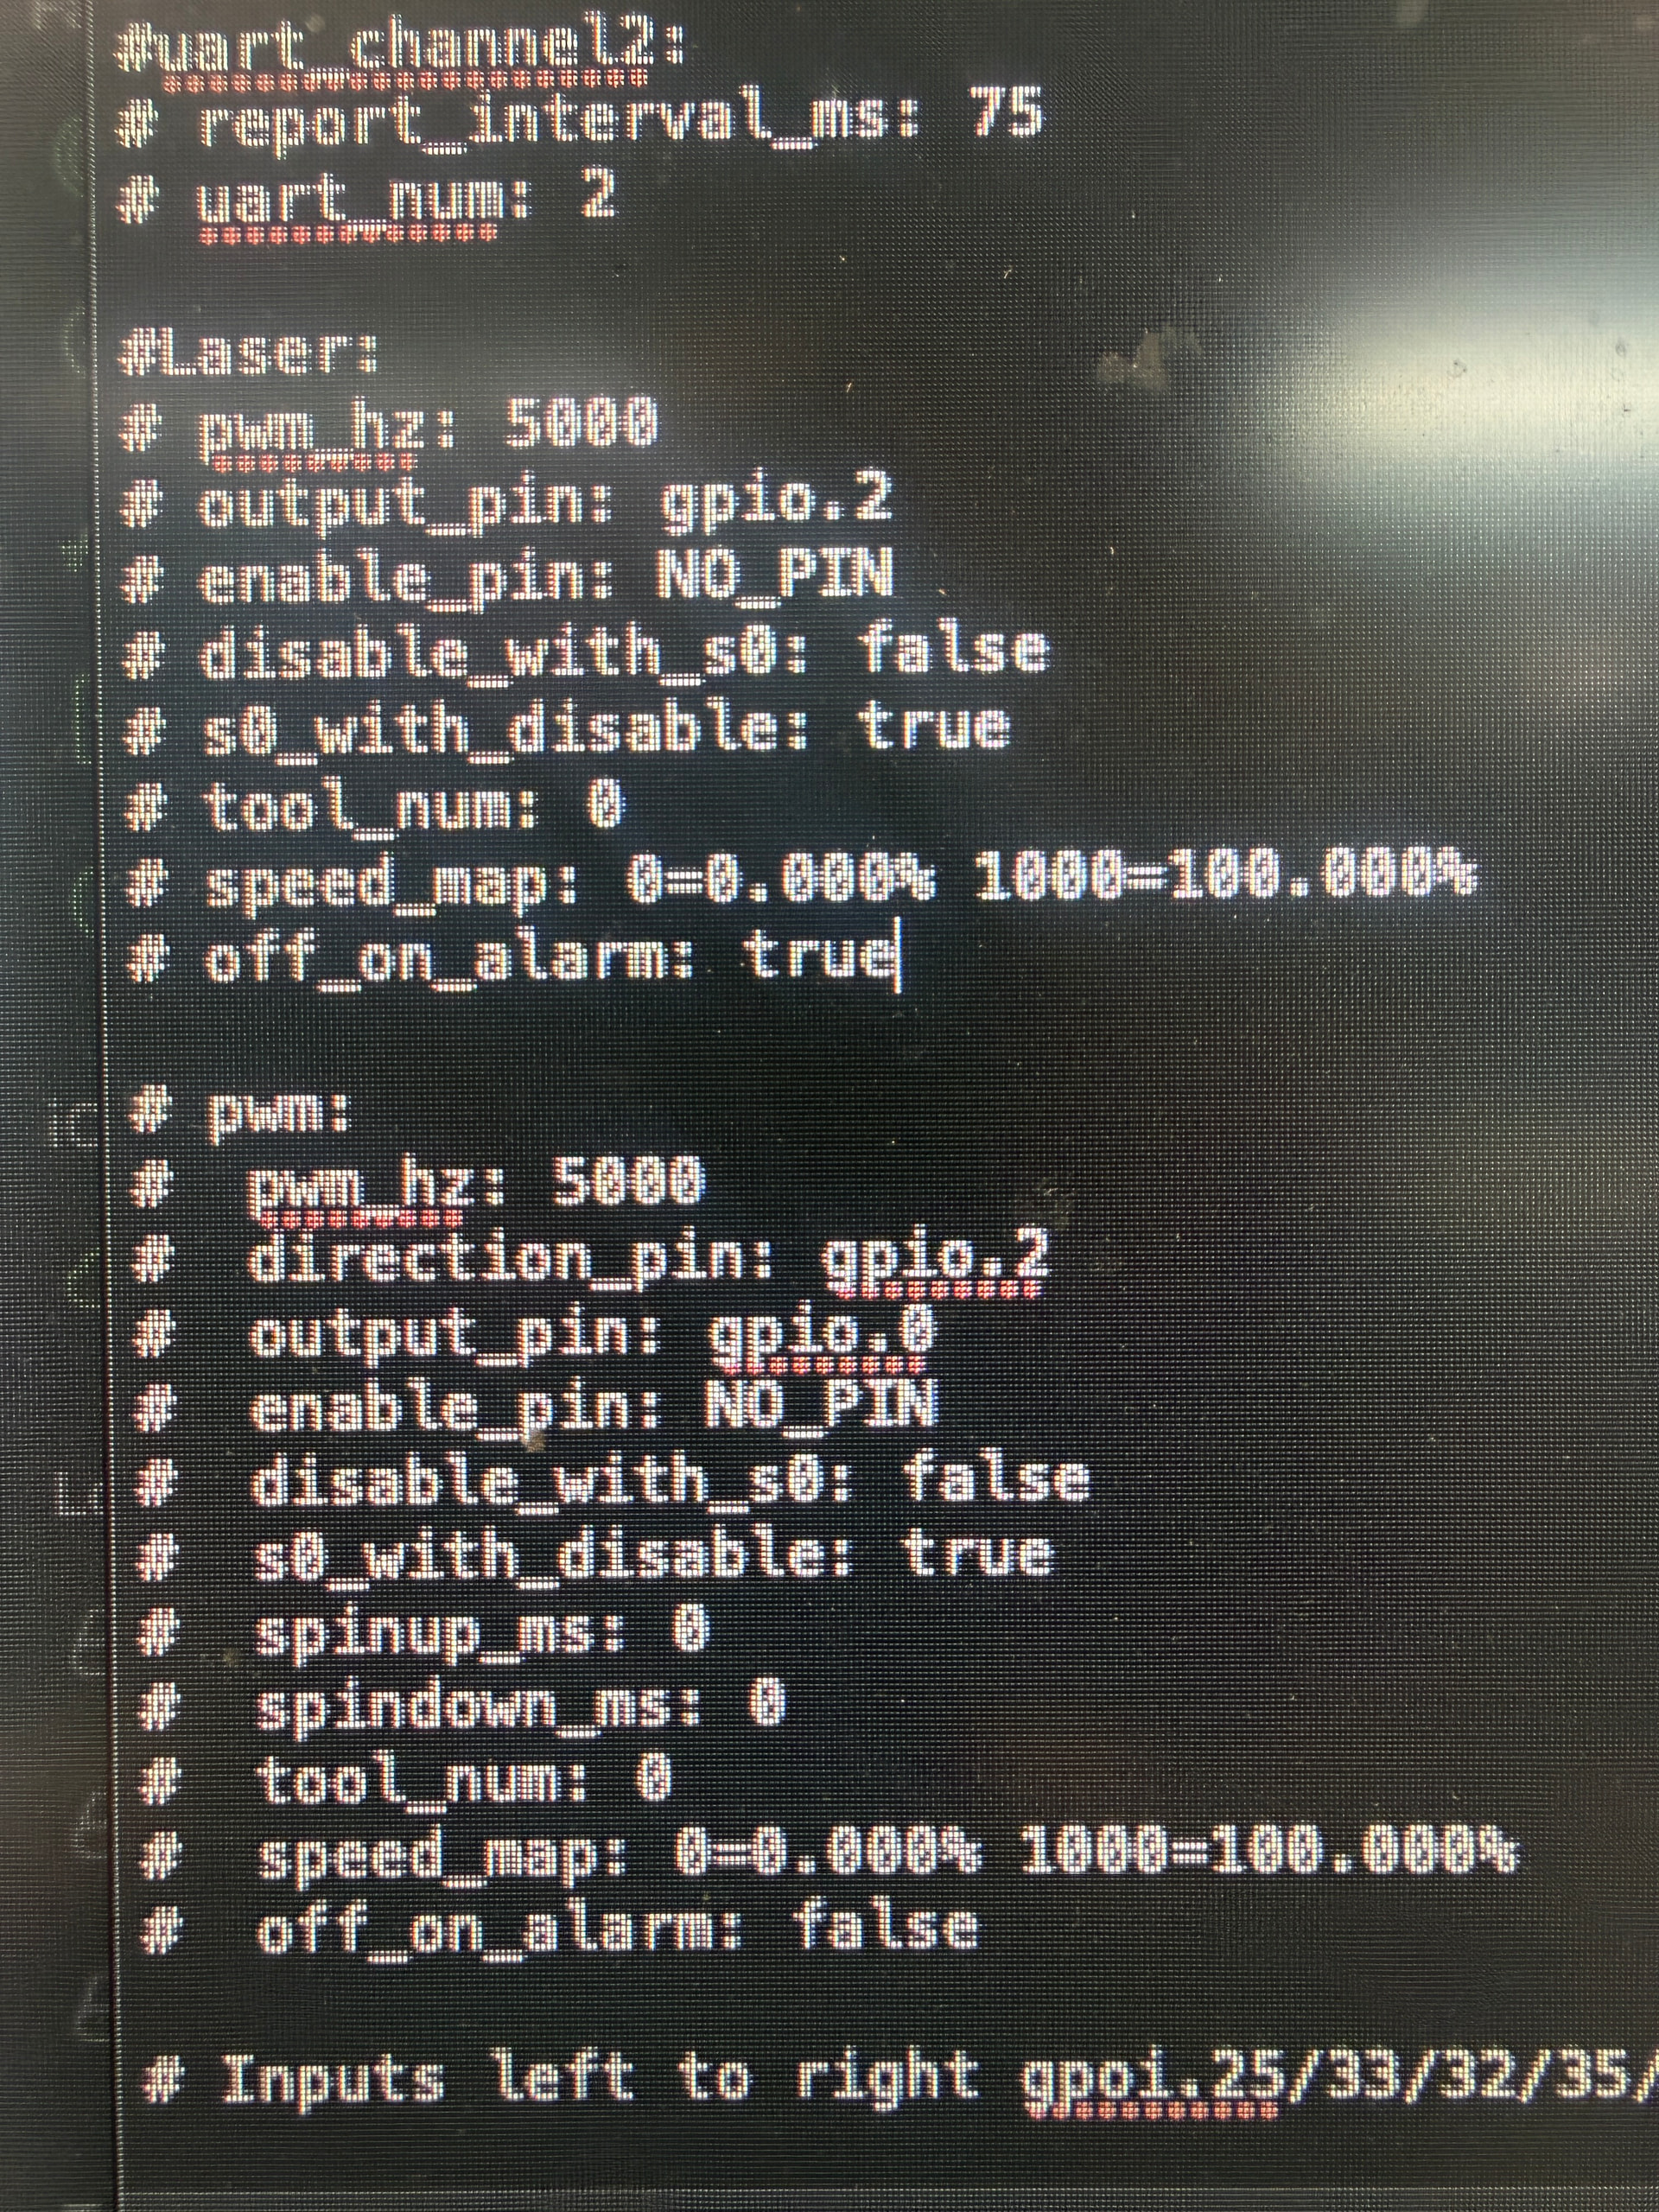
Sorry, that photo isn’t accurate, I have the # removed from the laser section.
your laser is commented out., remove the #
Sorry, the photo isn’t the most recent, the # is removed from the laser section.
Repeat your $$ with current settings.
Also see if this first section does the trick for you. No worries, I had the same issue when I first started. It should be a simple fix and maybe a little tuning.
you also dont need $32 for fluidnc, it will switch automatically to laser mode when the laser tool is selected
post the gcode here as well. are you using M3 or M4 mode ?
Here is the current photo, the pwm works great, I tried commenting it out and using the laser, and it will only fire at 100%. So I’m using the pwm. As far as the m code goes, in the device settings menu for grbl it does not show the m codes for the laser. When I look in the console neither m3 or m4 are used.
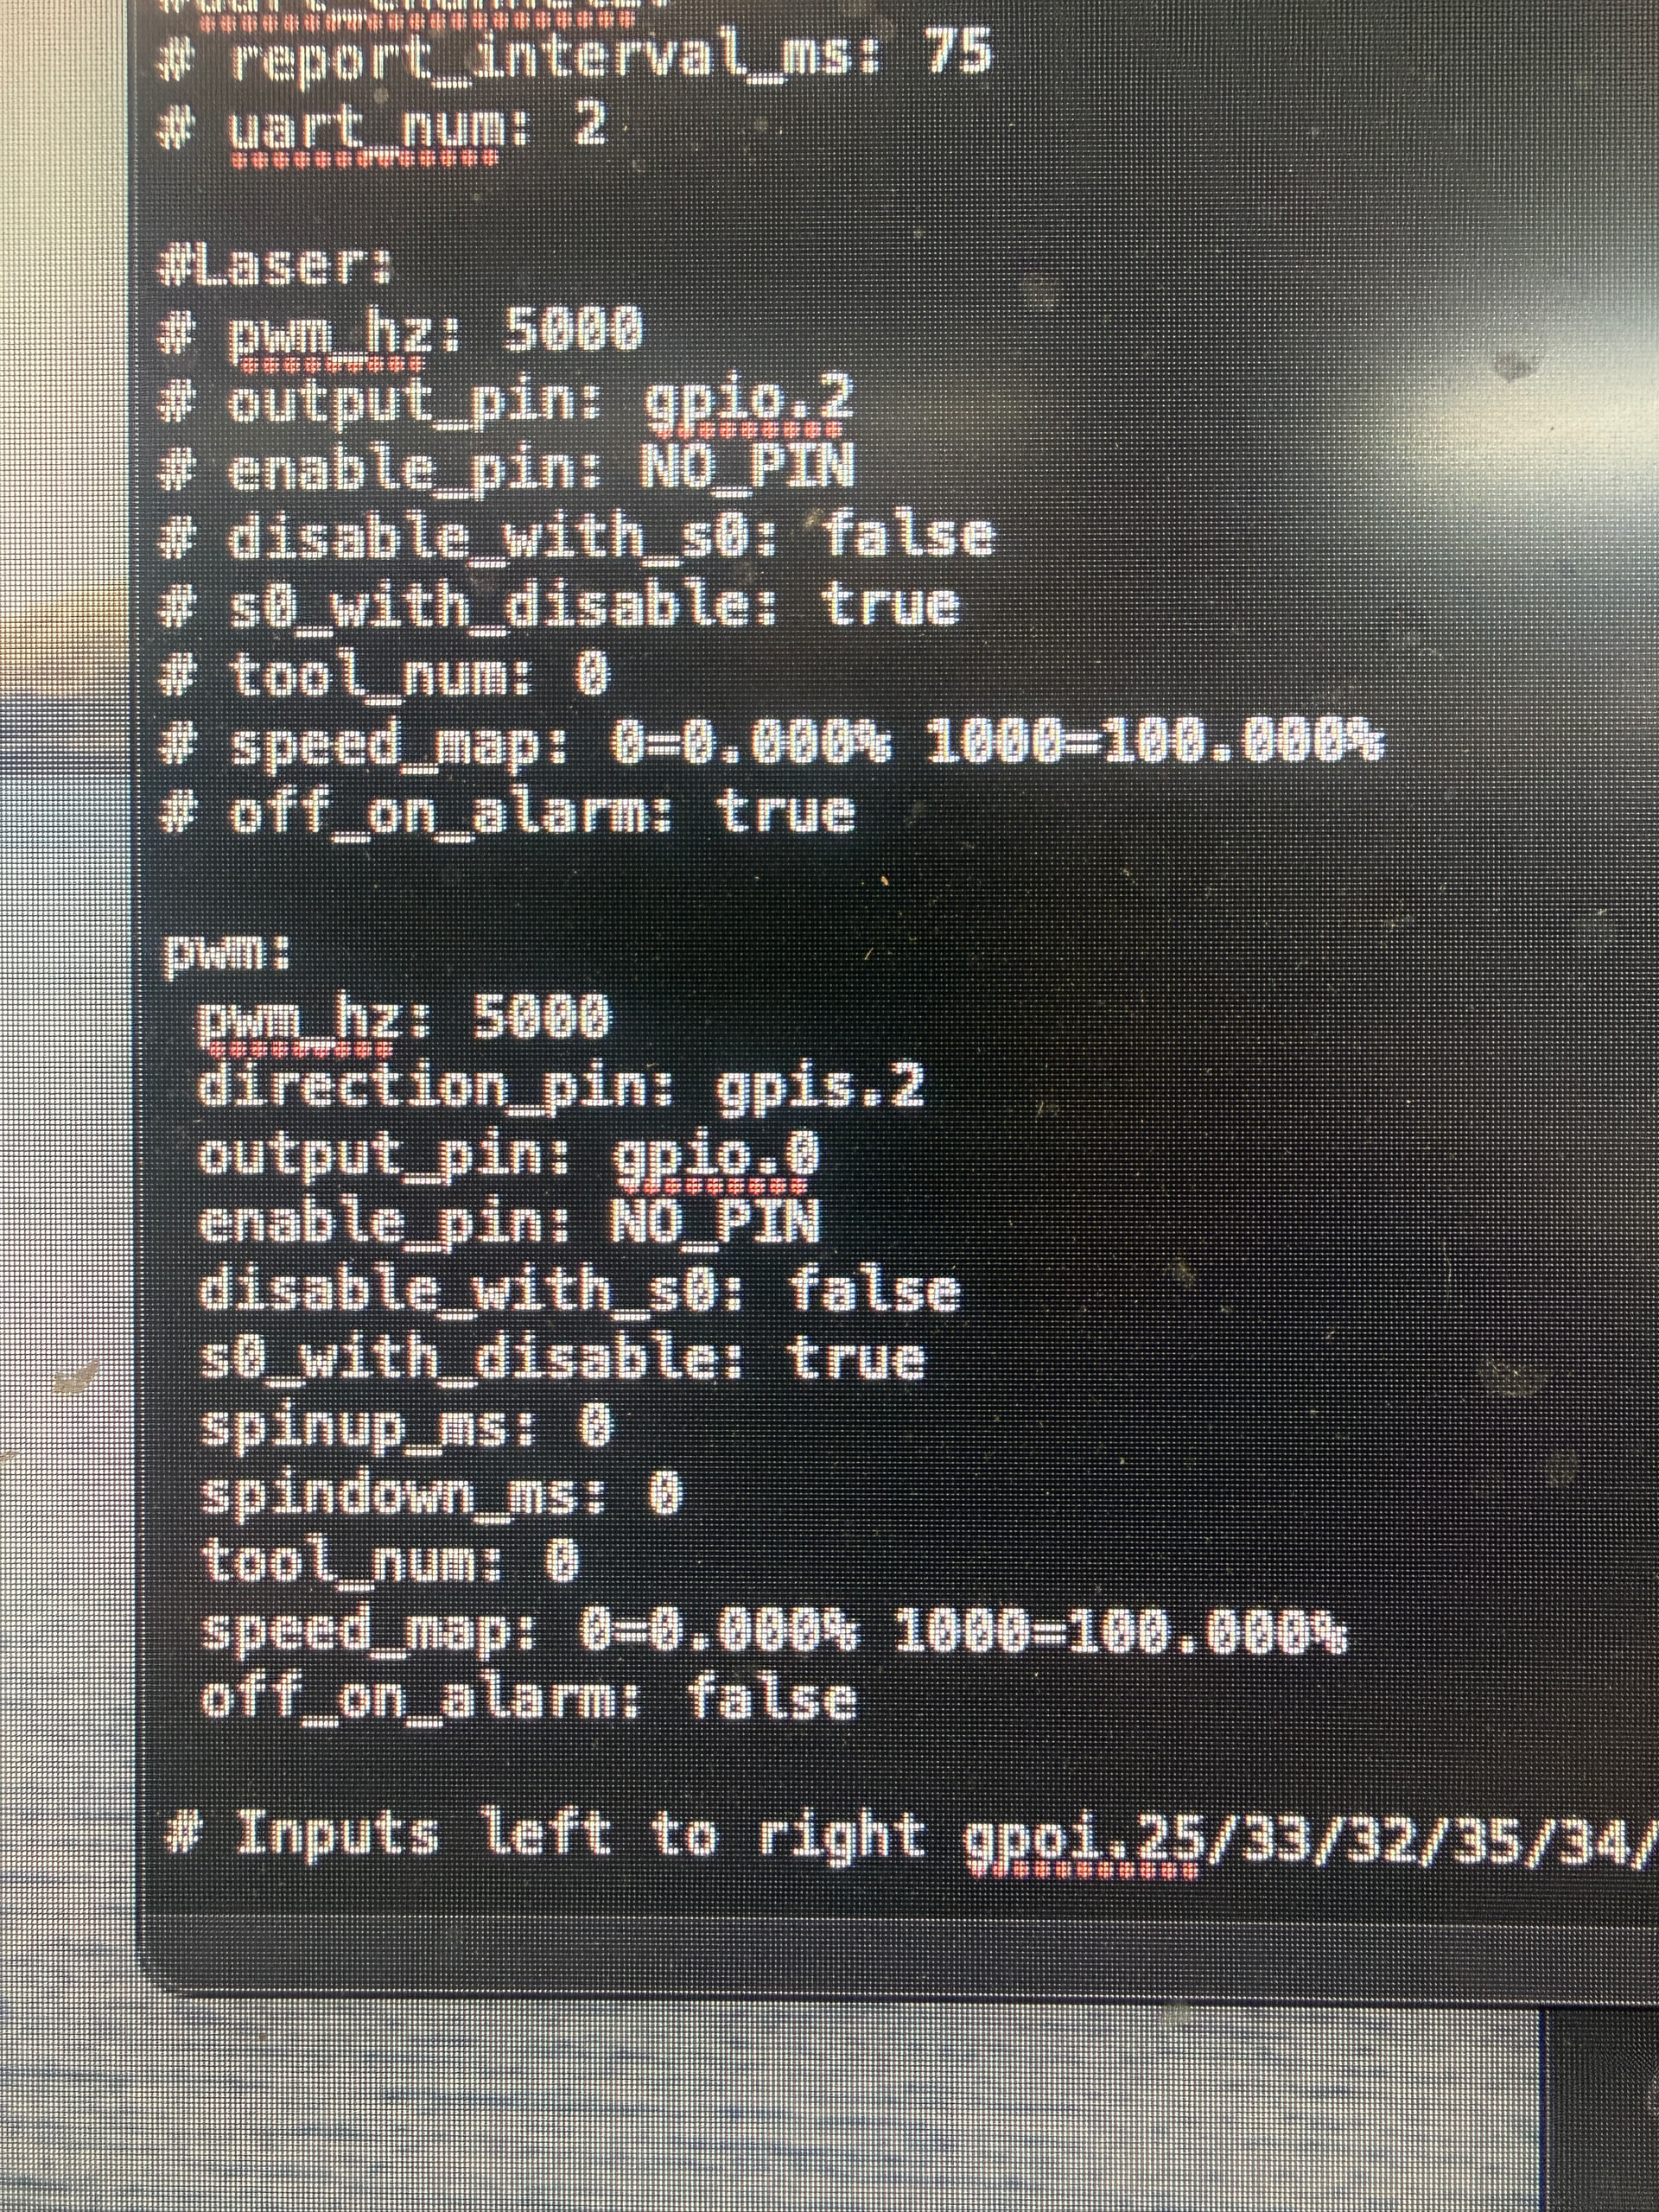
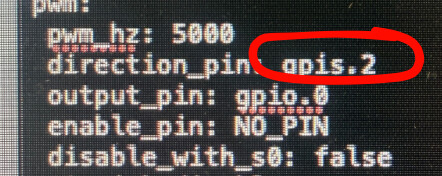
Looks like a typo, retype gpio.2
Here is my config.yaml, I use a different GPIO pin and use a 60W Lasertree but maybe you can gleam a few things.
Laser:
  pwm_hz: 5000
  output_pin: gpio.26
  enable_pin: NO_PIN
  disable_with_s0: false
  s0_with_disable: true
  tool_num: 10
  speed_map: 0=0.000% 100=13.000% 1000=100.000%
  off_on_alarm: true
  m6_macro:
EDIT: the speed mapping was custom to me, but that was the right curve to ensure I didn’t have burnt edges where the laser slows down for right edges, etc.
you’ll need to add M6 T10 at the top of your gcode to select the laser tool
i do the same thing on my one. i do not have laser mounted all the time but the config is there all the time
Yup, but thanks for reminding me. It was in my defaults when making anything in Lightburn, but tonight is the first time I am opening it since the new computer and really down that my settings are toast. I will have to rebuild my machine settings, luckily I took some notes.
My router and laser are set up in an IDEX format zeroed at the same point so I can build gcode to engrave and come back and cutout with the router.
I corrected the gpio.2 but that made no difference. I did not add the tool change line as my Mpcnc is a dedicated laser.
You should first run $SS to see if your config is valid.
I’ve checked in the webui and my configuration is set for a Mpcnc, pmw is enabled in the config file.
But that provides detail if the config is valid. If not, trying anything is futile. Do you have an MPCNC or a Lowrider?
I have a Mpcnc
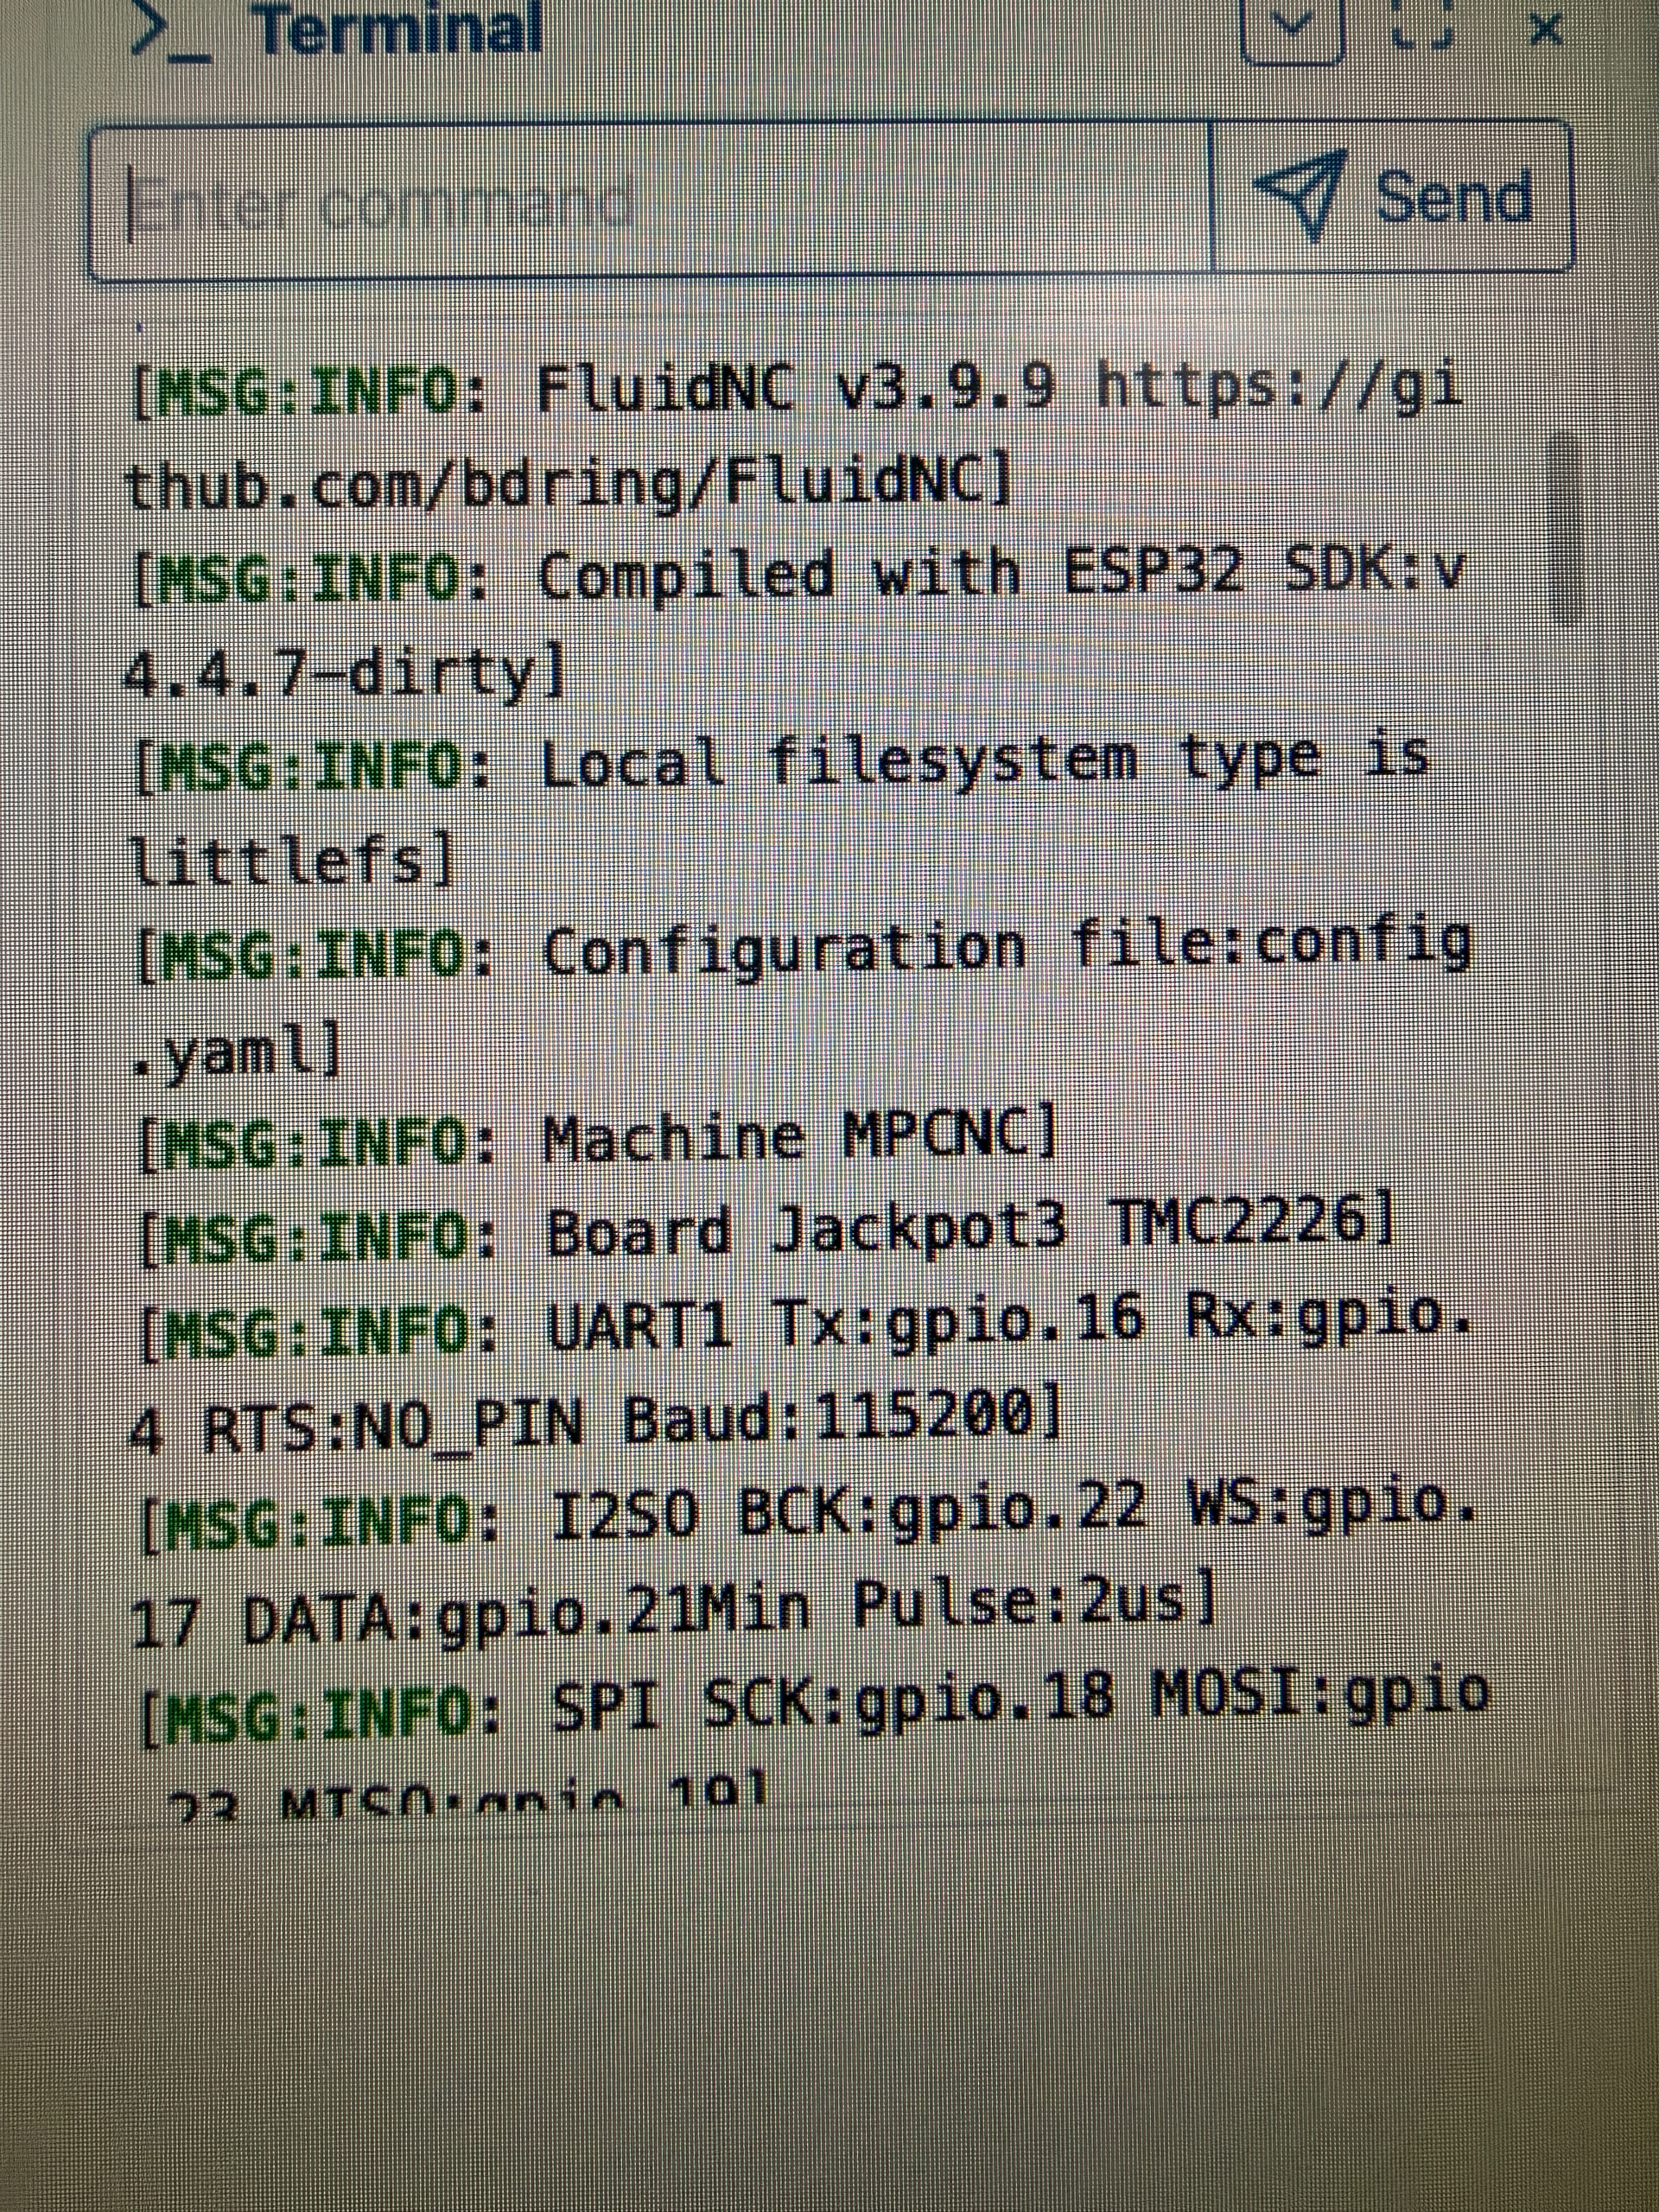
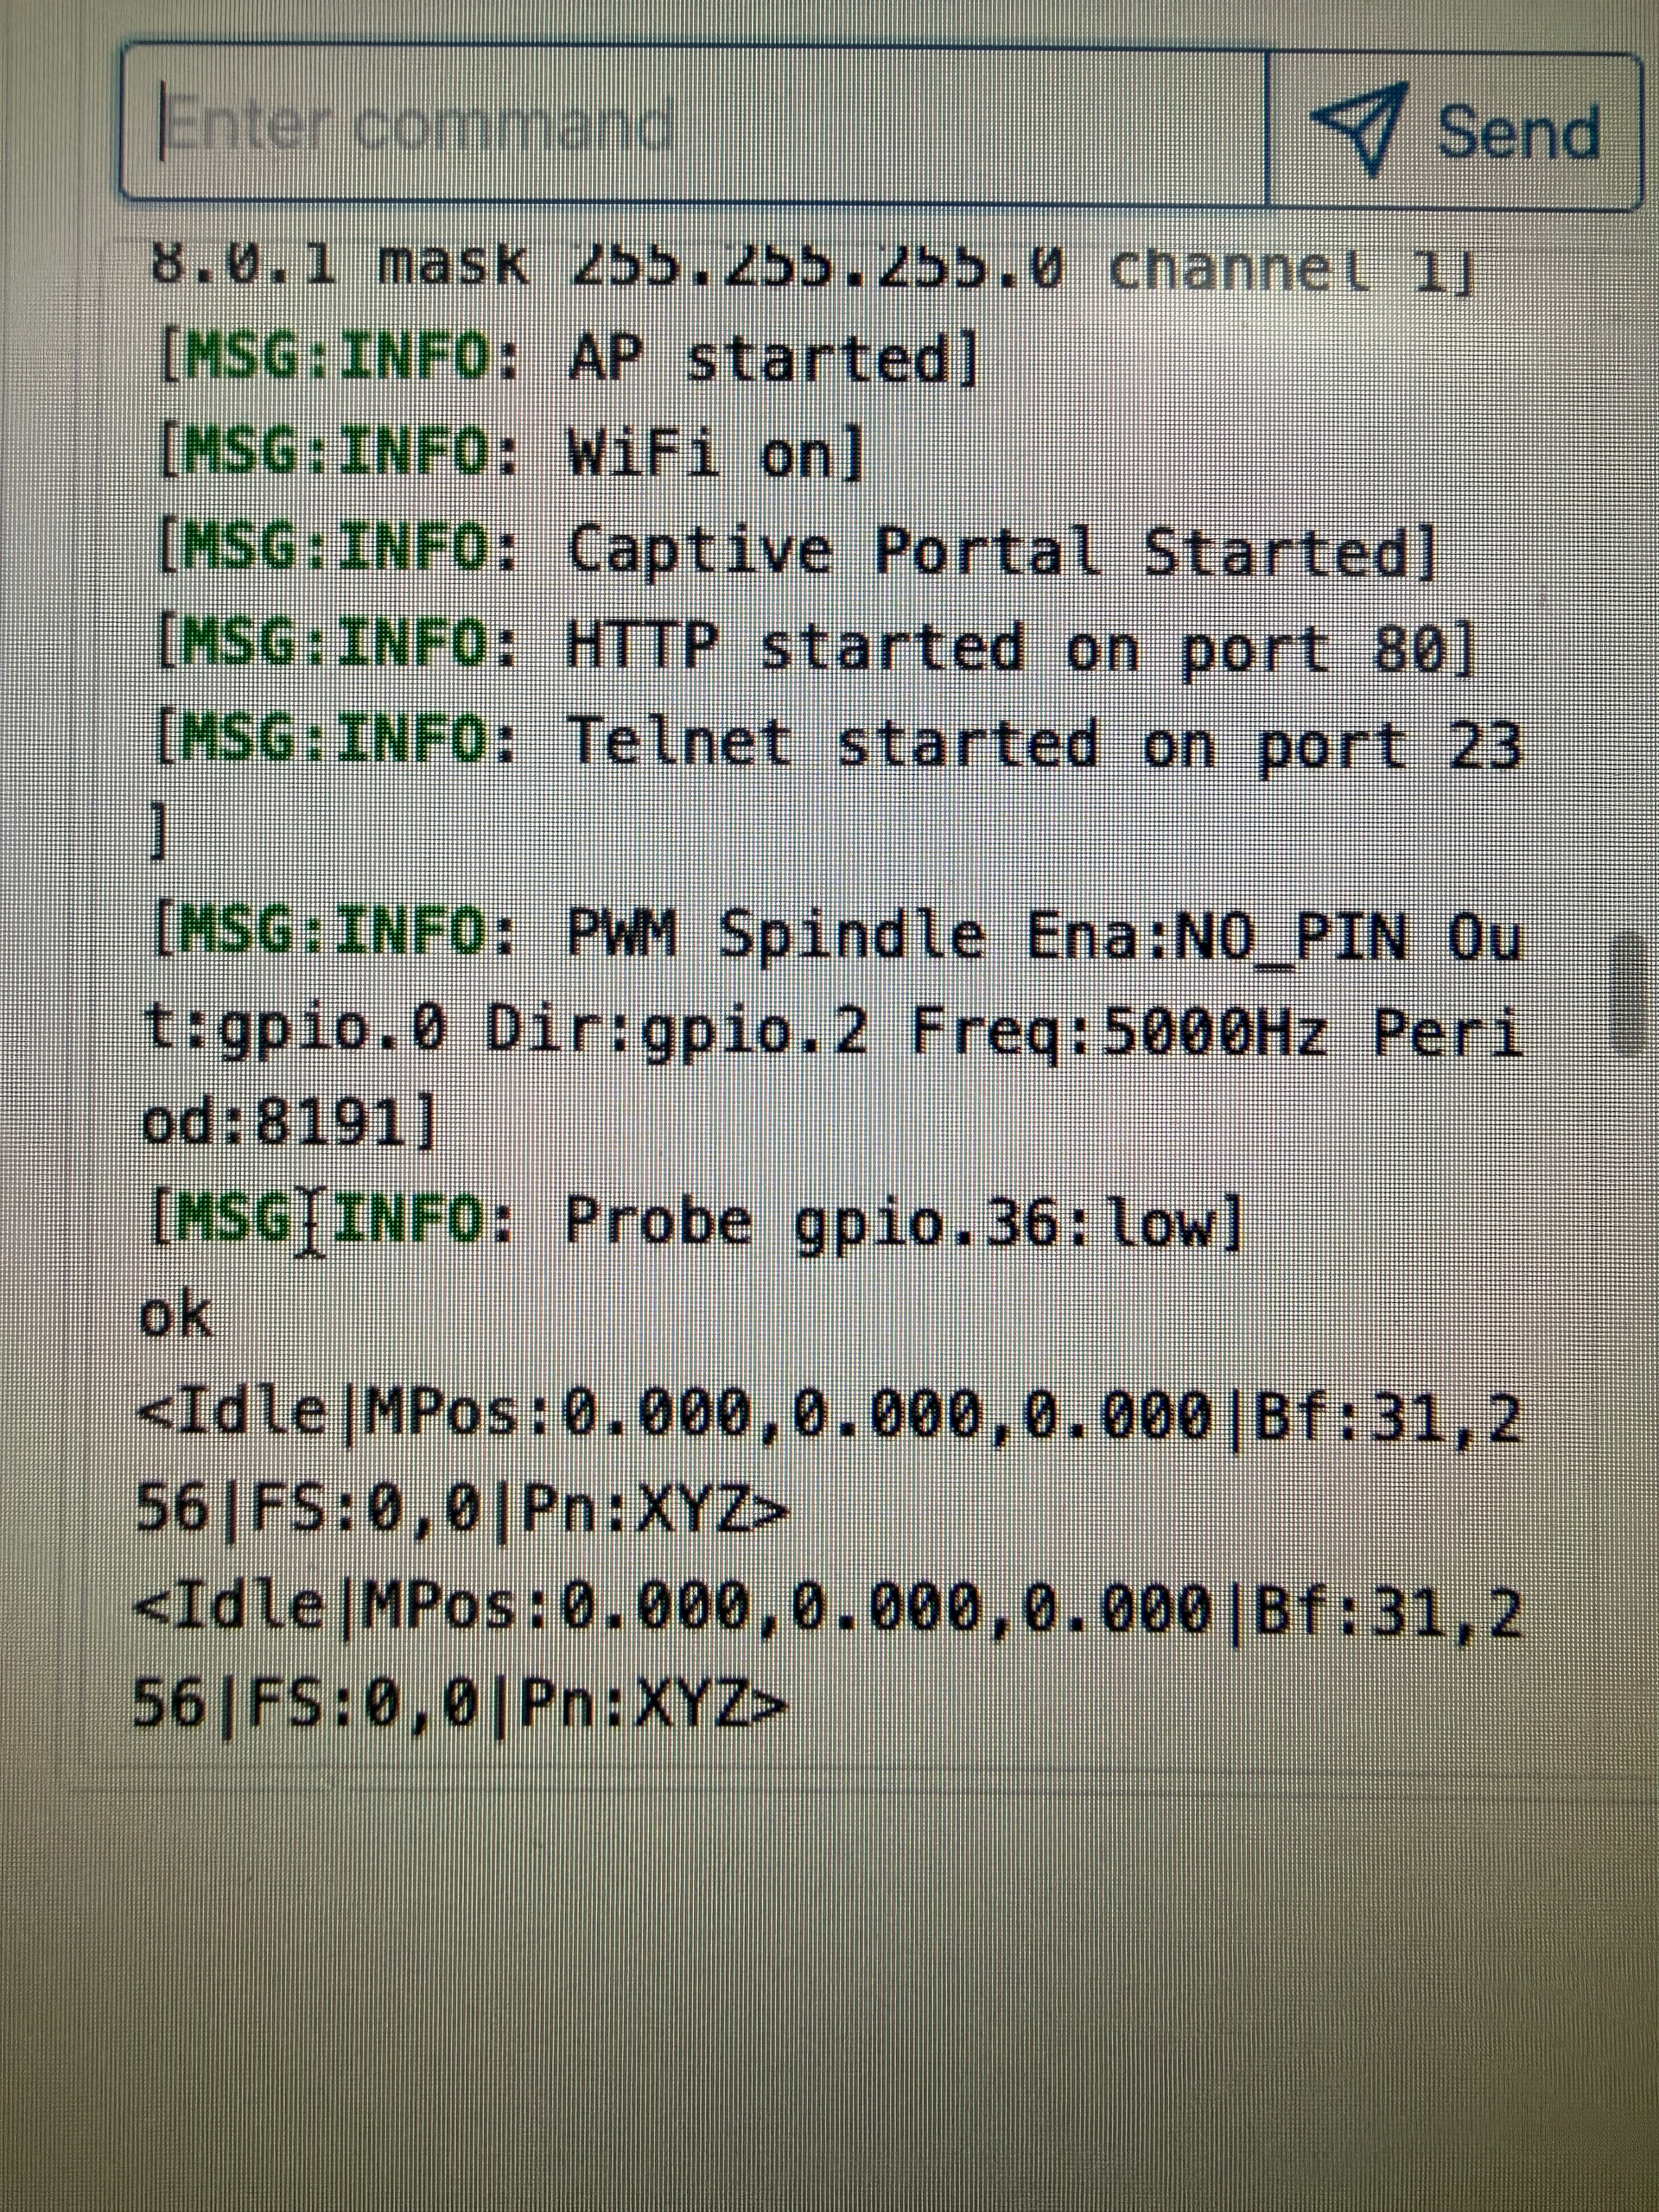
you need to be in laser mode to auto turn off the laser
if you can control the laser power in pwm spindle mode that means that the wiring is correct
what issues do you have when you try to use laser spindle ?